 Search
 en
 English
 日本語
 русский
 Español
 Deutsch
 中文简体
Content
- 1 Understanding the Function of an Optical Prism
- 2 Advantages of Precision Optical Prisms
- 3 Applications of Optical Prisms
- 4 Advanced Manufacturing Process for Optical Prisms
- 4.1 1. Technical Review and Optical Design Confirmation
- 4.2 2. Material Preparation and Inspection
- 4.3 3. Cutting, Blocking, and Preforming
- 4.4 4. Precision Grinding
- 4.5 5. Fine Grinding and Surface Preparation
- 4.6 6. Polishing
- 4.7 7. Edge Finishing and Chamfering
- 4.8 8. Cleaning and Surface Preparation
- 4.9 9. Optical Coating
- 4.10 10. Final Inspection and Documentation
- 5 Manufacturing Strengths That Differentiate a Professional Supplier
- 6 Optical Prism Performance Compared with Alternative Components
- 7 How to Specify a Custom Optical Prism
- 8 Quality Risks and How They Are Controlled
- 9 Why Choose Precision Optical Prisms from an Integrated Manufacturer?
- 10 Future Development of Optical Prism Technology
- 11 Frequently Asked Questions
- 11.1 What is an optical prism used for?
- 11.2 How is a prism different from a mirror?
- 11.3 Which materials can be used to manufacture optical prisms?
- 11.4 Why are prism angles so important?
- 11.5 What does surface quality mean for an optical prism?
- 11.6 Do all optical prisms require coatings?
- 11.7 Can optical prisms be customized?
- 11.8 What industries use precision optical prisms?
- 11.9 How can a manufacturer improve prism consistency?
- 11.10 What information should be included in an inquiry?
- 11.11 Why are ISO and automotive quality certifications valuable?
- 11.12 Can one supplier support both prototype and volume production?
- 12 Conclusion
- 13 References
- 14 Product: Optical prism
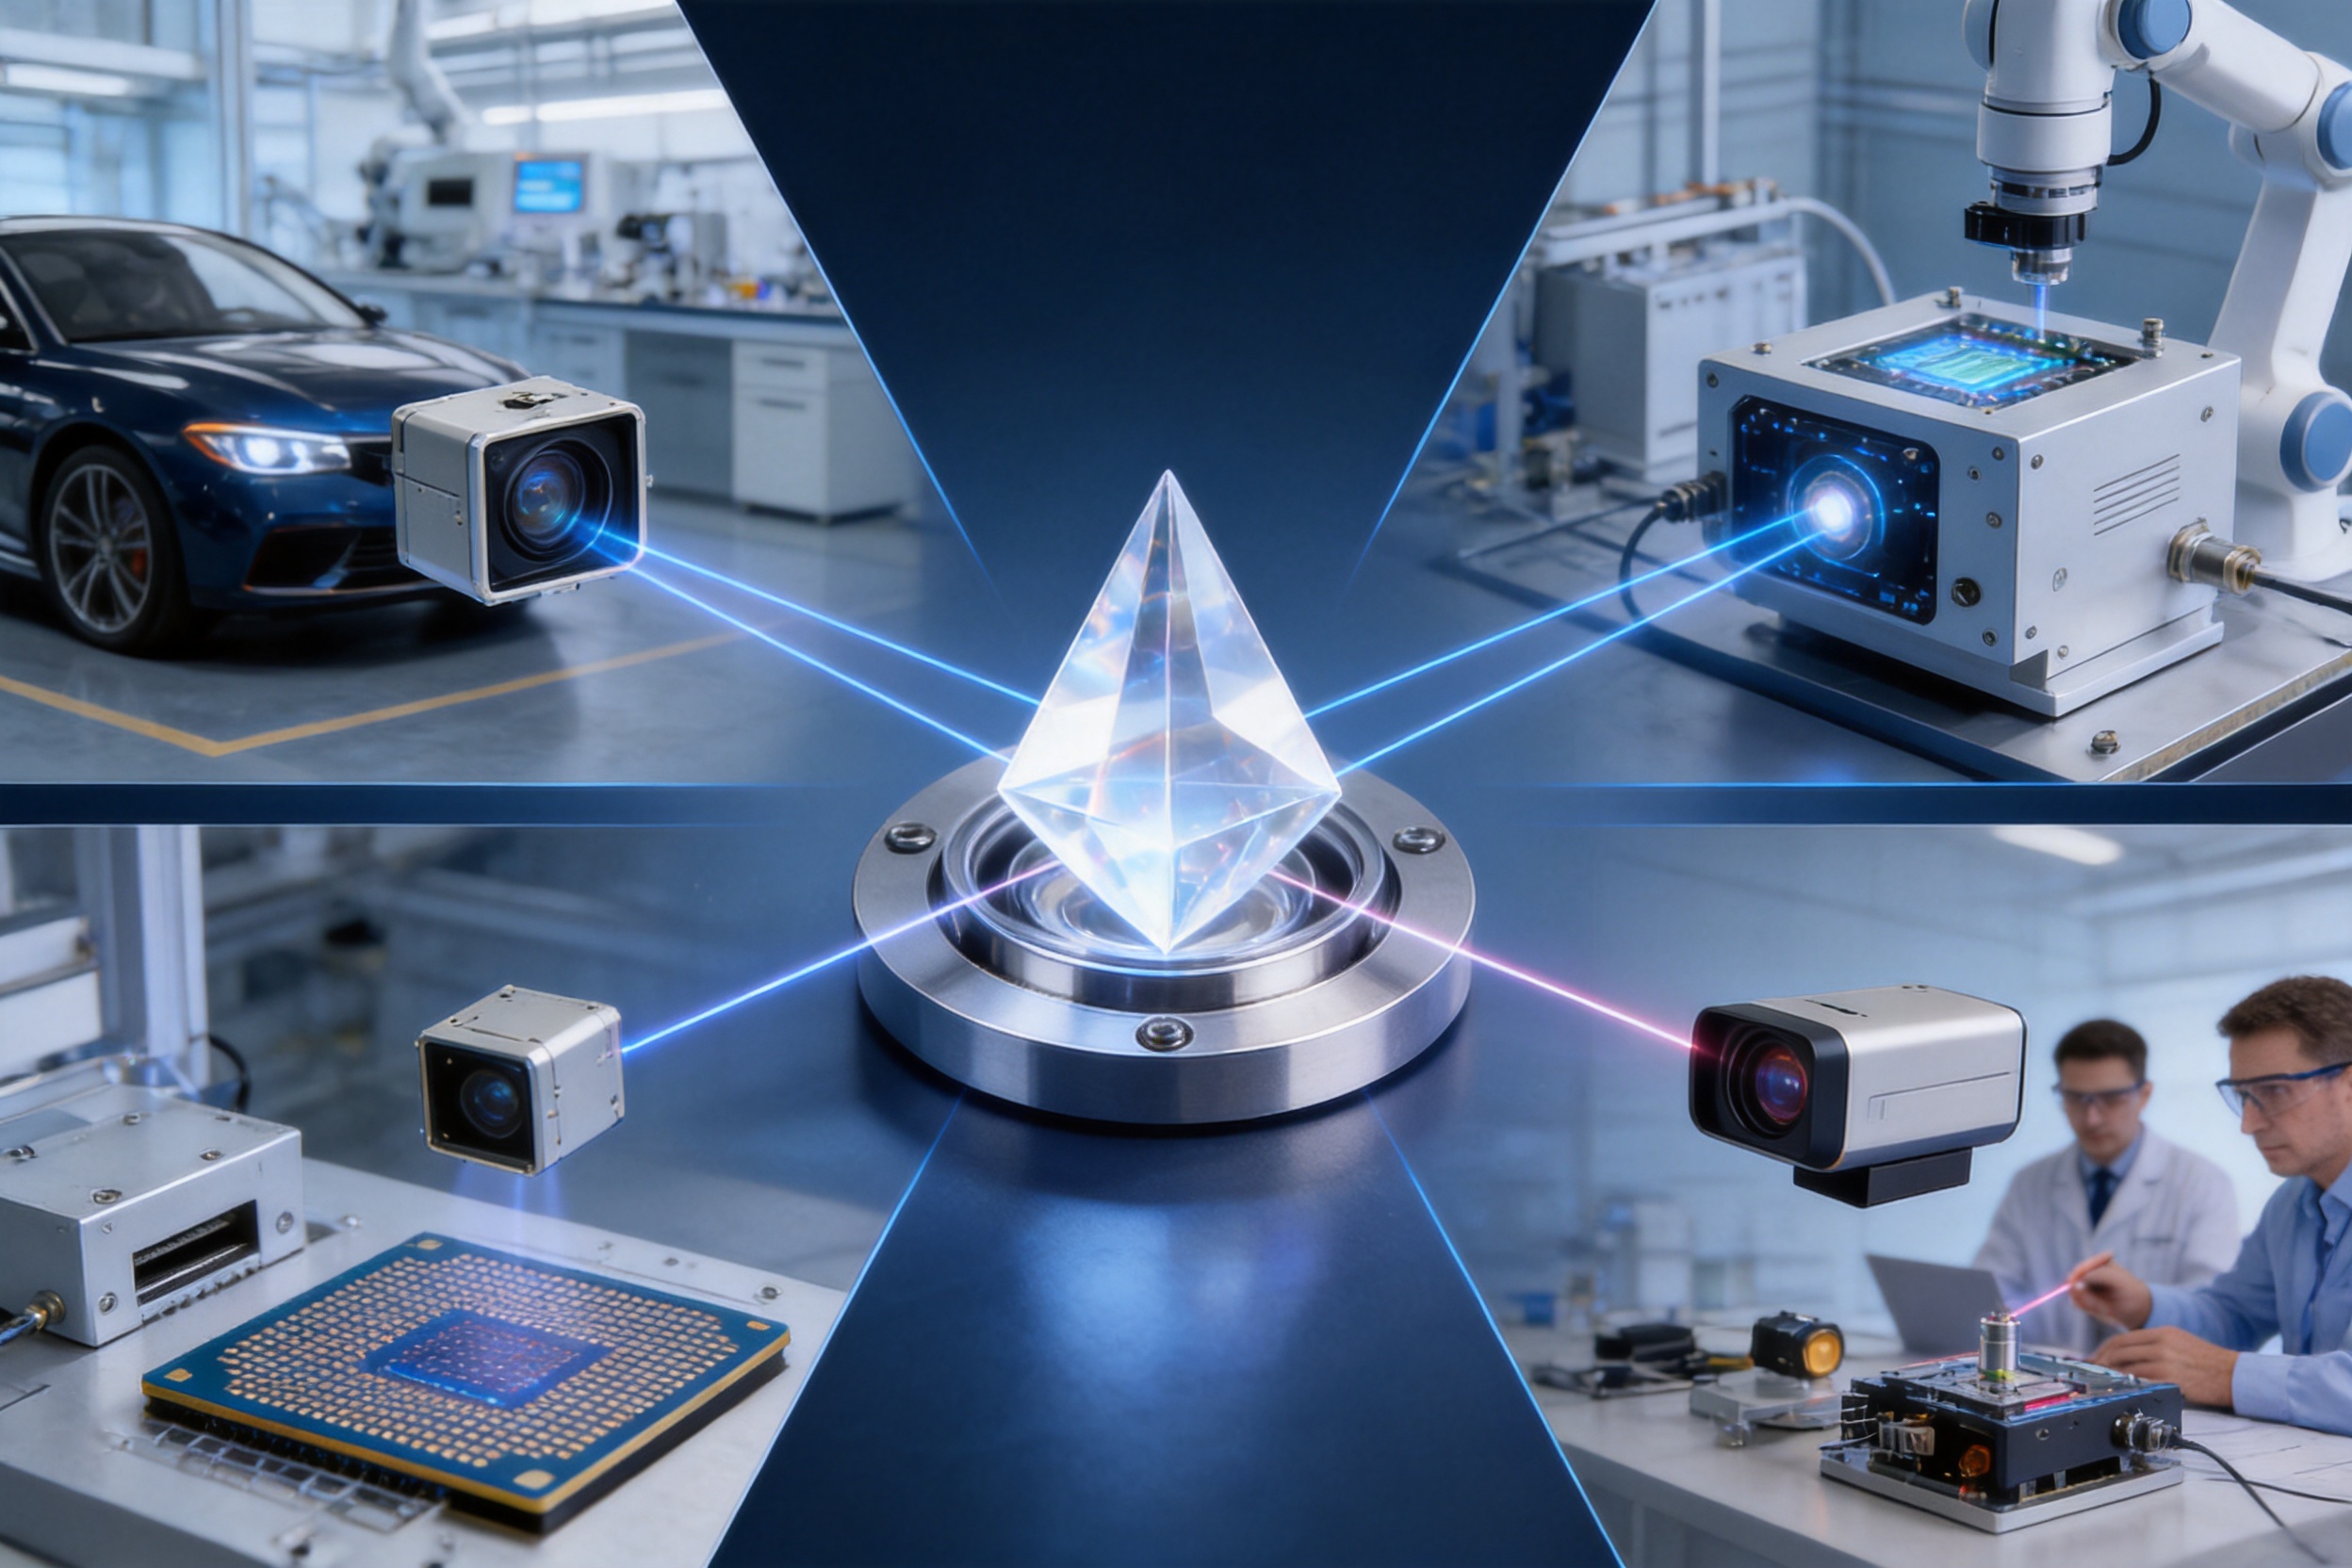
Optical prisms are precision components that control, redirect, separate, fold, or otherwise modify light through carefully engineered refractive and reflective surfaces. Although a prism may appear to be a simple geometric element, its performance depends on a complex combination of optical design, material quality, surface accuracy, angular precision, coating technology, cleanliness, and inspection discipline. In demanding optical systems, a small deviation in prism angle or surface flatness can affect beam alignment, image quality, polarization behavior, spectral performance, and long-term reliability.
Precision optical prisms are therefore manufactured according to strict process requirements rather than ordinary glass-processing methods. They must be designed for their intended wavelength range, incident angle, environmental conditions, and mechanical installation method. Depending on the application, a prism may be used for beam deviation, image rotation, dispersion, reflection, polarization control, or compact optical-path folding. The most reliable suppliers combine optical engineering expertise with stable production equipment, process control, coating capabilities, and comprehensive inspection.
Changzhou Haolilai Photo-Electricity Scientific and Technical Co., Ltd., commonly known as HLL, is a professional manufacturer of precision optical components established in 1998. Located in Changzhou, Jiangsu, China, the company operates from a facility covering approximately 35,000 square meters. Its capabilities include the development and production of precision optical components for laser optics, automotive optics, semiconductor optics, and consumer optics. Optical prisms are an important part of this product portfolio, supported by an experienced technical team, modern manufacturing systems, and quality-management certifications.
The following article explains the operating principles, advantages, manufacturing methods, quality factors, and application value of precision optical prisms. It also examines how an experienced optical component manufacturer can provide more consistent performance than suppliers relying on general-purpose glass processing or limited inspection procedures.
Optical prism
Understanding the Function of an Optical Prism
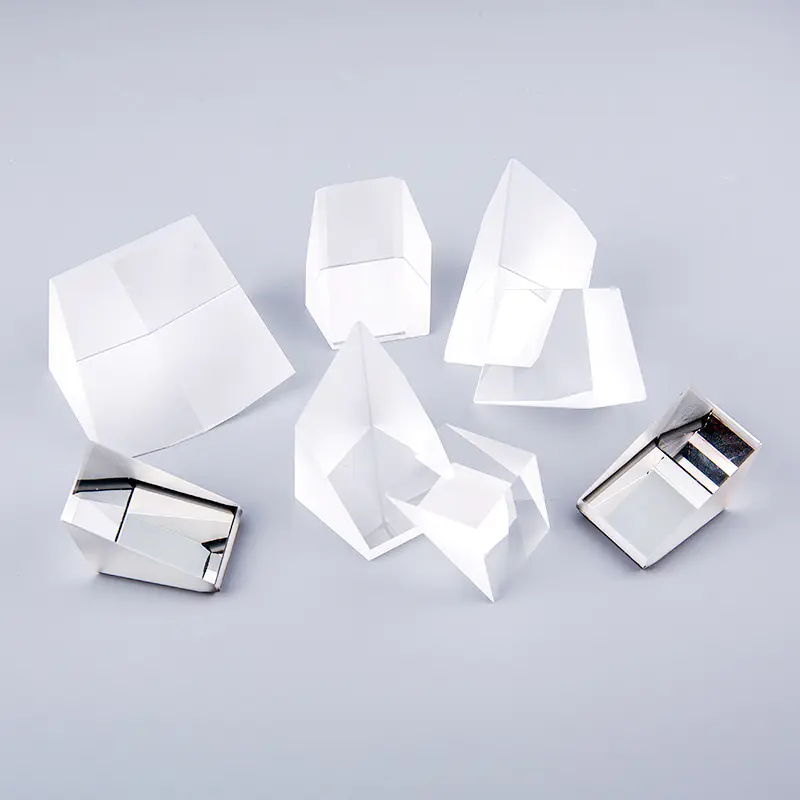
An optical prism is a transparent or reflective optical element with one or more precisely angled surfaces. When light enters a prism, its direction changes because of refraction at the interface between air and the optical material. The amount of deviation depends on the refractive index of the material, the angle of incidence, the prism geometry, and the wavelength of the light.
Prisms can also use total internal reflection or external reflective coatings to redirect light. This makes them valuable in compact optical systems where a mirror, lens group, or longer optical path would occupy more space. A prism can fold a beam around a corner, rotate an image, separate wavelengths, combine optical paths, or alter the orientation of a beam without adding electronic or mechanical components.
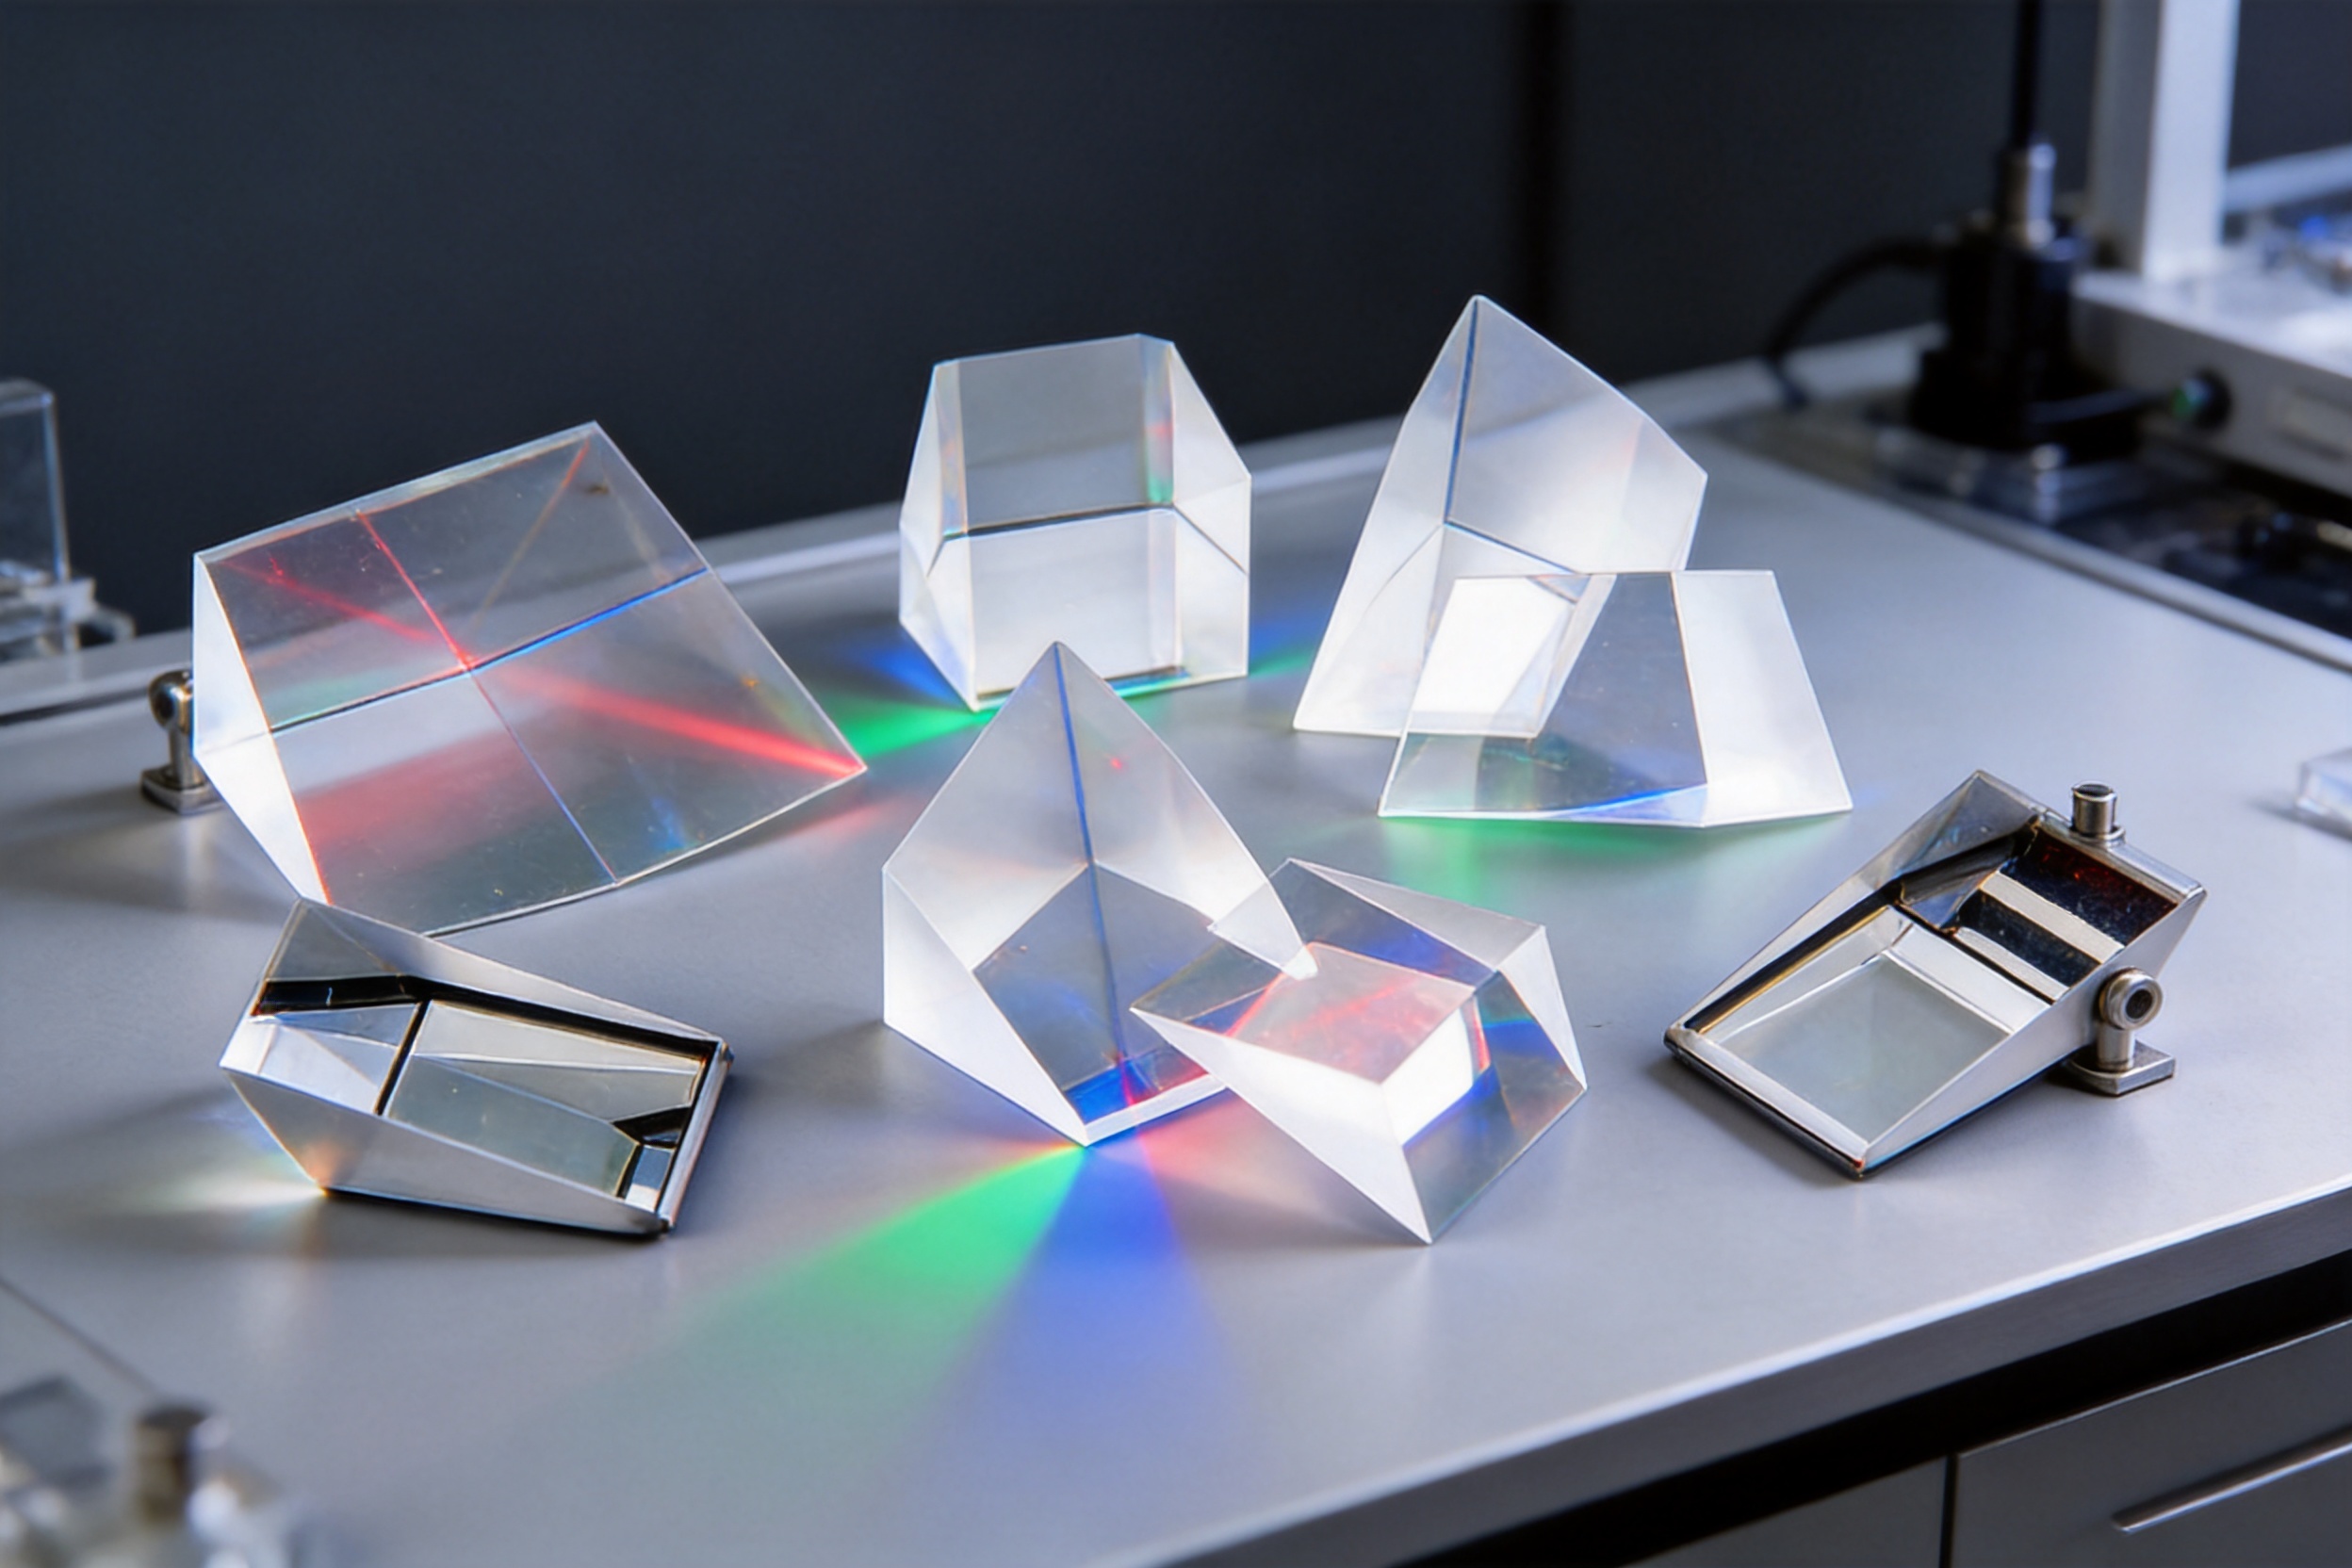
Common prism types include right-angle prisms, wedge prisms, Dove prisms, roof prisms, dispersing prisms, penta prisms, Porro prisms, retroreflecting prisms, and polarization prisms. Each type performs a different optical function. A right-angle prism may be used for beam deflection through 90 degrees, while a penta prism can maintain a nearly constant beam deviation even when the prism is slightly rotated. A wedge prism can intentionally change beam direction, and a dispersing prism can separate different wavelengths into an angular spectrum.
The name and geometry of a prism do not, by themselves, determine whether it is suitable for a particular instrument. The component must also meet requirements for transmission, reflection, surface quality, angular accuracy, coating durability, and resistance to its operating environment. For this reason, professional optical prism manufacturing begins with application analysis and optical specification review.
Key Optical Parameters
The most important optical prism parameters normally include material refractive index, Abbe number, wavelength range, angular deviation, clear aperture, surface flatness, surface roughness, wedge angle, chamfer dimensions, and coating performance. Depending on the design, the prism may also require specific polarization characteristics, low absorption, high laser-damage resistance, or low fluorescence.
Refractive index determines how strongly the material bends light. Abbe number indicates the degree of dispersion, or how much the refractive index changes with wavelength. These properties are especially important for prisms used in spectroscopy, imaging, laser systems, and color separation.
Surface flatness affects wavefront quality. A surface that is not sufficiently flat can introduce aberration, distort a transmitted image, or reduce the quality of a laser beam. Surface roughness affects scatter and stray light. Angular accuracy influences the final beam direction, while wedge error can cause unwanted beam deviation or image displacement.
Clear aperture is another important consideration. The usable optical area must be large enough for the beam or image field, while edge margins, chamfers, mounting areas, and potential coating boundaries must be considered during the design stage. A technically correct prism with an insufficient clear aperture may not perform properly after installation.
Advantages of Precision Optical Prisms
Precision optical prisms offer several advantages over less specialized beam-steering or image-forming components. Their value is not limited to the ability to redirect light. Properly designed prisms can improve system compactness, stability, optical efficiency, and alignment repeatability.
Compact Optical-Path Folding
One of the main advantages of a prism is its ability to fold an optical path within a small mechanical envelope. In a compact instrument, a prism can redirect light around a corner without requiring a separate mirror mount and adjustment mechanism. This can reduce the number of components, simplify assembly, and create a more rigid optical structure.
Compared with a conventional mirror mounted on a separate support, a prism may offer better mechanical integration. Its optical surfaces and mounting reference features can be designed as one component. When installed correctly, the resulting assembly can be less sensitive to vibration and accidental movement.
Stable Beam Deviation
Some prism designs provide highly stable beam deviation. For example, a penta prism can maintain a nominal beam deviation of approximately 90 degrees even when the prism is rotated around its axis within the intended operating geometry. This property is useful in surveying instruments, metrology systems, alignment equipment, and optical measurement devices.
The stability of beam deviation depends on the accuracy of the prism angles and the quality of the optical surfaces. A well-controlled manufacturing process helps ensure that the designed optical behavior is reproduced consistently from one batch to another.
Efficient Use of Total Internal Reflection
Prisms can be designed to use total internal reflection, allowing light to be redirected with very low loss when the relevant conditions are satisfied. This can be advantageous in systems where a reflective coating would introduce absorption, polarization changes, or long-term coating-maintenance concerns.
Total internal reflection is not automatically suitable for every application. The incident angle, refractive index, wavelength, surface cleanliness, and surrounding medium must all be considered. Nevertheless, when properly designed, a total-internal-reflection prism can provide an efficient and durable optical path.
Image Rotation and Orientation Control
Prisms are widely used for image rotation, inversion, and orientation control. Optical instruments such as viewing systems, rangefinders, imaging devices, and inspection equipment may require an image to be corrected or rotated before it reaches the detector or eyepiece.
Because image orientation is determined by prism geometry, the component can perform this function passively and reliably. This is often more compact than using multiple mirrors or a complicated lens group. The design must account for image quality, chromatic effects, internal reflections, and the orientation of the prism within the instrument.
Wavelength Separation and Spectral Control
Dispersing prisms separate light according to wavelength. This behavior is useful in spectrometers, analytical instruments, optical sensors, and research equipment. Different materials and prism geometries provide different dispersion characteristics, allowing the prism to be selected for a specific spectral range.
High-quality surfaces and carefully selected materials are essential for spectral applications. Surface defects, contamination, or improper polishing can create scattering and reduce the accuracy of the measured spectrum. Coatings may also be applied to improve transmission in a selected wavelength band.
Mechanical and Environmental Reliability
A prism integrated into a robust optical assembly can be highly resistant to vibration and mechanical displacement. This is particularly valuable in automotive, industrial, semiconductor, and field-deployed instruments. However, reliability is determined by more than the glass itself. It also depends on edge finishing, coating adhesion, thermal compatibility, mounting stress, and inspection procedures.
A manufacturer with experience in multiple precision-optics markets is better positioned to understand how optical components behave after assembly. For example, automotive applications may demand resistance to temperature cycling and vibration, while semiconductor applications may require extremely low contamination and stable optical performance. These different requirements influence design, cleaning, packaging, and final inspection.
Applications of Optical Prisms
Laser Optics
Laser systems often require highly accurate beam redirection, beam folding, polarization management, and compact optical layouts. A prism can redirect a laser beam within a rigid optical block or provide a defined angular relationship between optical subsystems.
Laser applications place demanding requirements on surface quality, coating quality, material homogeneity, and laser-induced damage resistance. Even microscopic contamination can absorb energy and create localized heating. For this reason, prism production for laser systems generally requires controlled polishing, careful cleaning, suitable coating design, and packaging that protects the component from particles and handling damage.
Depending on the wavelength and power level, the prism may be supplied with an antireflection coating, high-reflection coating, polarization coating, or specialized laser coating. Coating selection should be based on wavelength, angle of incidence, polarization state, power density, pulse duration, and environmental conditions.
Automotive Optical Systems
Automotive optical systems increasingly use cameras, sensors, head-up displays, driver-monitoring systems, lighting modules, and advanced driver-assistance technologies. Optical prisms can be used to fold optical paths, redirect images, support compact sensor architecture, or manage light distribution in a confined vehicle structure.
Automotive components must perform consistently under vibration, temperature changes, humidity, dust, and long service intervals. Dimensional consistency is important because the prism may be assembled into a high-volume module with limited adjustment capability. Small variations in angular deviation or surface quality can affect image alignment and system calibration.
HLL holds IATF16949 certification in addition to ISO9001:2015 and ISO14001:2015 certification. IATF16949 is associated with automotive quality-management requirements and provides a foundation for process discipline, traceability, risk management, and continuous improvement in automotive-related manufacturing. Certification does not replace product-specific testing, but it demonstrates an established framework for controlled production.
Semiconductor and Inspection Equipment
Semiconductor manufacturing and inspection equipment rely on precise optical paths, stable imaging, and controlled illumination. Prisms may be used in metrology instruments, wafer inspection systems, alignment modules, microscope assemblies, and laser-based processing equipment.
These environments can be especially sensitive to contamination, optical scatter, thermal drift, and dimensional variation. A prism may need a carefully defined clear aperture, low scatter, high transmission, and reliable behavior over extended operating periods. Clean handling and packaging can be as important as grinding and polishing accuracy.
For semiconductor applications, the production process may include strict cleaning procedures, controlled inspection areas, detailed documentation, and customized acceptance standards. The supplier must understand not only the optical specification but also the customer’s assembly environment and contamination-control expectations.
Consumer Optical Products
Consumer optical products include cameras, projection equipment, compact imaging devices, virtual and augmented reality systems, optical sensors, and other high-volume products. These applications often combine demanding performance expectations with strict cost, delivery, and consistency requirements.
Prisms used in consumer products must be manufactured efficiently without compromising essential optical characteristics. Stable tooling, repeatable processing, automated or semi-automated inspection, and well-organized production planning can help achieve the necessary balance between quality and cost.
Scientific and Measurement Instruments
Optical prisms are used in spectrometers, surveying instruments, rangefinders, microscopes, laboratory systems, and precision measurement equipment. In these applications, the prism may serve as a beam divider, image rotator, wavelength separator, or reference element.
Scientific and measurement equipment often requires detailed optical documentation. Customers may need information about material grade, coating spectral performance, angular deviation, surface quality, flatness, and inspection results. A professional manufacturer can support these requirements through technical communication and controlled quality records.
Advanced Manufacturing Process for Optical Prisms
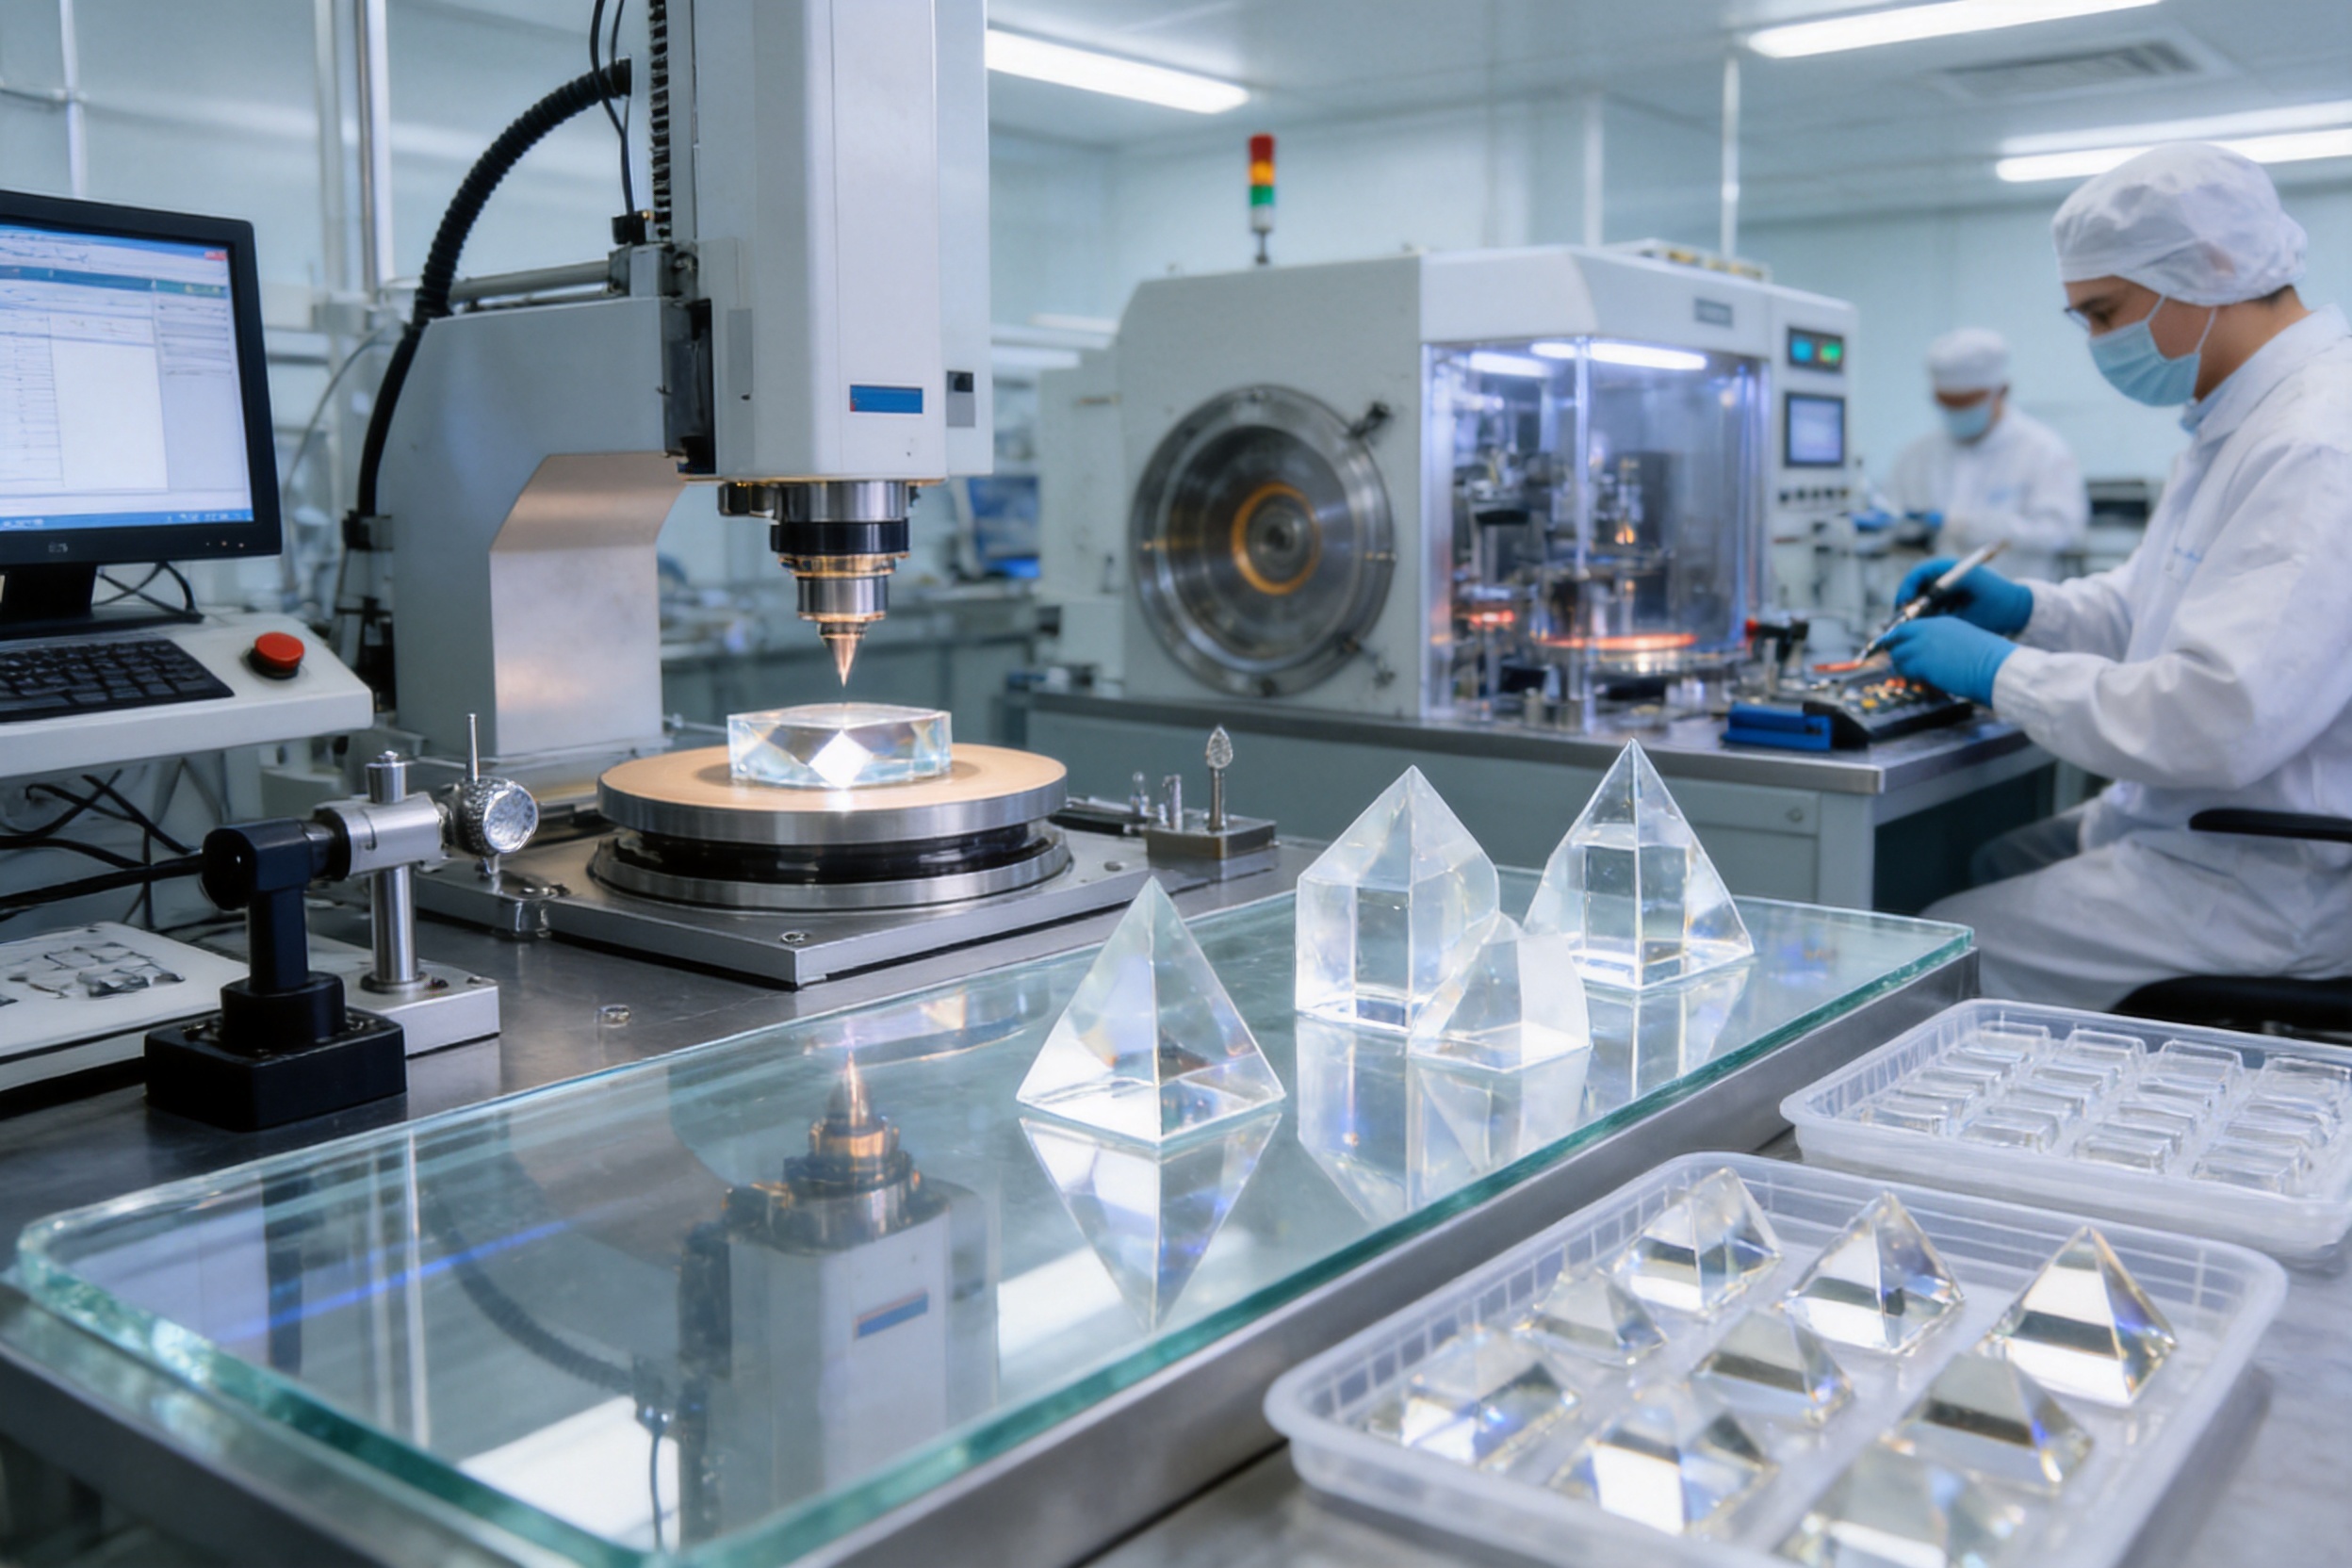
The manufacturing of a precision optical prism is a multi-stage process. Each stage influences the final result, and process stability is essential because errors introduced early in production may be difficult or impossible to remove later.
1. Technical Review and Optical Design Confirmation
Production begins with a review of the customer’s drawings, optical specifications, material requirements, quantity, application, and environmental conditions. This review should identify critical dimensions, reference surfaces, coating requirements, tolerances, inspection methods, and packaging expectations.
For a prism, the relationship between mechanical dimensions and optical angles is especially important. The manufacturer must understand which surfaces are functional, which edges are mounting references, and how the prism will be oriented in the final assembly. Design-for-manufacturing feedback at this stage can reduce production risk and improve yield.
Material selection is also confirmed during the technical review. Optical glass, fused silica, crystalline materials, and other transparent media each have different refractive properties, thermal behavior, hardness, polishing characteristics, and coating compatibility. The appropriate material depends on wavelength, power, environmental conditions, and cost objectives.
2. Material Preparation and Inspection
Optical material is inspected before processing. Typical checks may include dimensions, visible defects, bubbles, inclusions, striae, refractive-index consistency, and material identification. Material with unsuitable internal defects can reduce transmission or create unwanted scatter, particularly in laser and imaging applications.
Material preparation also includes cutting or blanking the glass into suitable starting pieces. The blank must provide enough allowance for grinding and polishing while minimizing unnecessary material waste. Proper orientation may be important for certain materials or optical designs.
3. Cutting, Blocking, and Preforming
During cutting and preforming, the material is shaped close to the final prism geometry. Diamond tools or other precision-processing equipment may be used to establish the basic dimensions and angular relationships. At this stage, the objective is to remove material efficiently while controlling subsurface damage.
Blocking or fixturing holds the workpiece in a stable position during subsequent operations. The fixture must support the part without introducing excessive stress or distortion. For small or complex components, fixture design has a direct influence on repeatability and production efficiency.
4. Precision Grinding
Grinding establishes the prism’s principal geometry, surface angles, thickness, and reference dimensions. Coarse grinding removes cutting damage, while finer grinding prepares the surfaces for polishing. The process must control both material removal and angular relationships.
For prism production, angular accuracy is critical because the final beam deviation depends directly on the relationship between the surfaces. Grinding equipment, tooling, abrasives, coolant conditions, and measurement procedures must be coordinated to prevent cumulative errors.
Grinding also affects the depth and distribution of subsurface damage. If the grinding stage is too aggressive or poorly controlled, polishing may require excessive material removal. This can reduce dimensional stability and increase production time.
5. Fine Grinding and Surface Preparation
Fine grinding reduces surface irregularities and prepares the optical surfaces for polishing. The abrasive size, pressure, speed, and processing time must be selected according to the material and the desired surface quality.
At this stage, operators and engineers monitor flatness, angle, thickness, and appearance. Measurement results guide process adjustments and help prevent defective parts from advancing to later operations. Early detection is more efficient than discovering a dimensional issue after coating or final assembly.
6. Polishing
Polishing produces the required optical smoothness, surface quality, and wavefront performance. It is one of the most sensitive steps in optical manufacturing because the process must remove remaining surface damage while preserving the prism’s geometry.
Polishing tools may be selected according to surface shape, part size, material, and production volume. Process parameters can include polishing compound, tool pressure, relative speed, temperature, and time. The objective is to achieve a smooth surface with low scatter and controlled figure error.
Maintaining prism angles during polishing requires careful control. Uneven removal can change the designed geometry, resulting in angular deviation or wedge error. Skilled process engineers use inspection data to compensate for predictable polishing behavior and improve consistency across batches.
7. Edge Finishing and Chamfering
Edges are finished to remove sharp corners, reduce chipping risk, and provide appropriate mechanical clearance. Chamfers must be controlled because they can affect the usable clear aperture and the way the prism is mounted.
Proper edge finishing also improves handling safety and reduces the possibility of edge damage during cleaning, coating, transportation, or assembly. The dimensions and appearance of chamfers may be specified on the engineering drawing and should be inspected accordingly.
8. Cleaning and Surface Preparation
After polishing, the prism is carefully cleaned to remove polishing residue, particles, oils, and other contaminants. Cleaning methods depend on the optical material, coating requirements, and intended application.
Cleaning is not simply a cosmetic step. Residual contamination can interfere with coating adhesion, increase scatter, create absorption sites, or cause visible defects in an assembled optical system. Professional handling practices reduce the risk of recontamination after cleaning.
9. Optical Coating
Coatings are applied when the prism requires improved transmission, reflection, polarization performance, or environmental protection. Antireflection coatings can reduce Fresnel losses at transmitting surfaces, while reflective coatings can improve beam redirection when total internal reflection is not appropriate.
Coating design must consider wavelength, angle of incidence, polarization, substrate material, operating temperature, humidity, power level, and cleaning requirements. A coating that performs well at one wavelength may not be suitable for another. Likewise, a coating designed for low-power imaging may not withstand a high-energy pulsed laser.
Coating quality depends on substrate cleanliness, vacuum-system condition, deposition control, layer thickness accuracy, adhesion, and post-coating inspection. Coated prisms should be handled and packaged in a manner that protects the optical surfaces from scratches and particles.
10. Final Inspection and Documentation
Final inspection verifies that the prism meets the approved drawing and technical specification. Depending on the product, inspection may include dimensional measurement, angular deviation, surface flatness, surface quality, clear aperture, coating performance, transmission, reflection, appearance, and cleanliness.
Inspection equipment should be selected according to the optical function of the component. Coordinate measurement, interferometric methods, optical benches, spectrophotometers, visual inspection, and specialized angle-measurement equipment may all be used in a comprehensive quality program.
Documentation can include inspection reports, material certificates, coating test results, batch identification, and conformity records. Traceability is valuable for both high-volume production and customized engineering projects because it supports root-cause analysis and continuous improvement.
Manufacturing Strengths That Differentiate a Professional Supplier
Optical prism performance is influenced by the entire manufacturing system, not by one machine or one operator. A supplier’s competitive advantage comes from the integration of engineering, production, inspection, quality management, and customer support.
Long-Term Optical Manufacturing Experience
HLL was founded in 1998 and has more than two decades of experience in precision optical-component manufacturing. Long-term experience supports the development of process knowledge for different glass types, prism geometries, coatings, inspection requirements, and application environments.
Experience is particularly valuable for custom products. A standard catalog specification may not fully describe the optical or mechanical requirements of a new system. Experienced engineers can identify potential manufacturing risks, recommend practical tolerances, and help customers balance performance with production cost.
Dedicated Technical and Engineering Resources
The company has an experienced technical team and has established the Jiangsu Precision Optical Lens Engineering Technology Center and the Jiangsu Enterprise Technology Research Center. These technical resources support product development, process improvement, application analysis, and the development of new optical-component solutions.
For optical prism customers, engineering support can include drawing review, material selection, tolerance analysis, coating discussions, prototype planning, and production scale-up. This technical cooperation is important when the prism is a critical element in a larger optical assembly.
Quality and Environmental Management
HLL has obtained ISO9001:2015 and ISO14001:2015 certifications, as well as IATF16949 certification. ISO9001 provides a framework for quality-management processes, customer requirements, corrective action, and continual improvement. ISO14001 focuses on environmental-management practices. IATF16949 supports disciplined quality management for automotive-related production.
These certifications are valuable because they encourage documented procedures, defined responsibilities, process monitoring, internal audits, and structured improvement. For customers, a formal management system can provide greater confidence that production is controlled beyond the inspection of individual parts.
Broad Industry Coverage
HLL develops and produces precision optical components for laser optics, automotive optics, semiconductor optics, and consumer optics. This broad application range allows the company to work with different requirements for optical accuracy, environmental reliability, cleanliness, production volume, and cost control.
Knowledge gained in one sector can support improvements in another. For example, automotive process discipline can benefit high-volume production, while semiconductor optical requirements can encourage stronger contamination control. Laser-optics experience can contribute to improved surface and coating management.
Large Production Base and Workforce
The company’s approximately 35,000-square-meter facility and workforce of more than 300 employees provide a foundation for production capacity, engineering coordination, inspection, and customer service. Facility scale can be particularly useful when customers require both prototype development and subsequent volume production.
A larger and organized manufacturing base can also support separate process areas, specialized equipment, material management, quality laboratories, and controlled packaging. The exact production arrangement depends on the product and customer requirements, but the overall infrastructure helps support stable delivery.
International Supply Experience
HLL exports to more than 20 countries and holds more than 30 certificates and patents. International supply experience requires attention to technical documentation, packaging, logistics, customer communication, quality expectations, and delivery coordination.
For overseas customers, an experienced export supplier can reduce communication risks during drawing confirmation, sampling, inspection approval, and repeat ordering. Clear documentation and consistent identification are especially important when the optical prism is incorporated into a global production program.
Optical Prism Performance Compared with Alternative Components
| Component or Method | Typical Strength | Considerations Compared with a Precision Prism |
|---|---|---|
| Optical prism | Compact beam deviation, image rotation, wavelength separation, and potential use of total internal reflection | Requires precise angles, careful polishing, suitable material selection, and controlled inspection |
| Front-surface mirror | Efficient reflection and flexible beam steering | May require a separate mount, alignment adjustment, and protective management of the reflective coating |
| Lens group | Focusing, collimation, magnification, and imaging functions | Usually cannot replace a prism’s compact beam-folding or image-orientation function without additional elements |
| Reflective coating on a flat substrate | Simple reflective path control | Performance depends strongly on coating durability, angle of incidence, polarization, and substrate flatness |
| Electronic or mechanical beam steering | Dynamic control and programmable positioning | Can increase system complexity, power consumption, cost, and sensitivity to mechanical or electronic failure |
The best component depends on the optical system. A prism is not universally superior to a mirror or lens, but it can provide an excellent combination of compactness, passive stability, optical efficiency, and multifunctional performance. The decision should be based on beam size, wavelength, power, environmental conditions, available space, alignment requirements, and production volume.
How to Specify a Custom Optical Prism
Customers preparing a prism inquiry should provide as much technical information as possible. A complete specification allows the manufacturer to evaluate feasibility, select materials, recommend tolerances, and estimate production requirements.
Recommended Specification Information
The drawing should identify the prism type, overall dimensions, optical surfaces, mechanical reference surfaces, angular tolerances, thickness tolerances, chamfer requirements, and clear aperture. If the component is used in a specific assembly, the drawing should also show the intended mounting orientation or reference datums.
Optical information should include operating wavelength or wavelength range, transmission or reflection requirements, beam diameter, polarization state, laser power if applicable, and expected wavefront or image-quality performance. If a coating is required, the specification should identify the coating function and spectral band.
Environmental information may include temperature range, humidity, vibration, vacuum exposure, chemical exposure, cleaning method, and expected service life. These details are particularly important for automotive, semiconductor, industrial, and outdoor applications.
Production information should include prototype quantity, annual demand, required delivery schedule, packaging needs, inspection documentation, and any special traceability requirements. Early communication about production volume can help the supplier select suitable tooling and process methods.
Quality Risks and How They Are Controlled
Several common defects can affect optical prism performance. These include chips, scratches, digs, polishing marks, haze, coating pinholes, angular errors, wedge, incorrect dimensions, contamination, and internal material defects. Each type of defect requires a specific prevention or detection method.
Angular errors are controlled through accurate grinding, stable fixturing, repeated measurement, and process compensation. Surface defects are reduced through appropriate polishing conditions and careful handling. Coating defects are controlled through cleaning, deposition monitoring, equipment maintenance, and post-coating inspection.
Contamination is controlled through cleaning, controlled handling, suitable protective materials, and packaging. Internal defects are addressed through material inspection and supplier control. Dimensional errors are reduced through calibrated measurement equipment, defined inspection plans, and process capability monitoring.
Quality control is most effective when it is preventive rather than purely corrective. A supplier should identify critical process parameters, establish acceptance criteria, record results, and use trend analysis to detect variation before it causes a large number of nonconforming parts.
Why Choose Precision Optical Prisms from an Integrated Manufacturer?
An integrated manufacturer can coordinate engineering, material preparation, shaping, polishing, coating, inspection, and packaging within one quality system. This reduces the risk of communication gaps between separate subcontractors and makes it easier to trace the origin of a problem.
Integrated production can also shorten development cycles. Customers can discuss the design with an engineering team, evaluate prototypes, adjust specifications, and transfer the approved product to volume manufacturing through the same organization. This continuity is especially useful for custom prisms that require repeated optimization.
HLL’s combination of long-term manufacturing experience, technical centers, quality certifications, broad industry coverage, patents, international supply experience, and a large production facility provides a strong foundation for optical prism production. Its focus on precision optical components supports the development of products for demanding applications rather than general-purpose glass products.
Another advantage is the ability to support different customer priorities. A research customer may require a small quantity of highly customized prisms and detailed inspection data. An automotive customer may prioritize repeatability, traceability, and process capability. A consumer-optics customer may require competitive pricing and high-volume consistency. A professional supplier should be able to adapt its process and documentation to these different needs.
Future Development of Optical Prism Technology
Optical prism applications are expected to continue expanding as optical systems become smaller, more integrated, and more intelligent. Automotive sensing, compact laser modules, semiconductor inspection, augmented-reality devices, industrial imaging, and advanced measurement systems all create demand for components that manage light within limited spaces.
Future prism development may involve more complex geometries, higher-performance coatings, improved spectral control, lower scatter, tighter angular tolerances, and greater integration with mechanical mounting features. New materials and surface-processing technologies may also expand the usable wavelength range and environmental performance of prism components.
Manufacturers will need to improve not only optical performance but also production efficiency, digital traceability, environmental responsibility, and rapid customization. A company with established technical resources and formal quality systems is well positioned to respond to these trends.
Frequently Asked Questions
What is an optical prism used for?
An optical prism is used to redirect, fold, rotate, separate, combine, or otherwise control light. Common functions include 90-degree beam deviation, image inversion, image rotation, wavelength dispersion, polarization control, and compact optical-path folding.
How is a prism different from a mirror?
A mirror redirects light primarily through reflection, while a prism normally uses refraction, total internal reflection, external reflection, or a combination of these effects. A prism can provide compact integration and may reduce the need for a separate mirror mount. A mirror may offer more flexible beam steering, especially when adjustable alignment is required.
Which materials can be used to manufacture optical prisms?
Material selection depends on wavelength, refractive index, dispersion, transmission, thermal behavior, laser power, environmental conditions, and cost. Optical glass is common, while fused silica, crystalline materials, and other optical media may be selected for specialized applications.
Why are prism angles so important?
Prism angles determine beam deviation, image orientation, dispersion, and the relationship between the optical component and the rest of the system. Small angular errors can produce beam misalignment, image displacement, or reduced system accuracy.
What does surface quality mean for an optical prism?
Surface quality describes the presence and size of scratches, digs, polishing marks, pits, and other surface imperfections. High surface quality reduces scatter and supports better imaging, transmission, and laser performance.
Do all optical prisms require coatings?
No. Some prisms are designed to use total internal reflection and may not require a reflective coating on the relevant surface. Other prisms need antireflection, high-reflection, polarization, or protective coatings. The correct choice depends on wavelength, angle of incidence, power, polarization, and environmental requirements.
Can optical prisms be customized?
Yes. Prisms can be customized in geometry, dimensions, material, surface quality, angular tolerance, clear aperture, coating, chamfer design, packaging, and inspection documentation. Customization should be discussed during the technical review so that the design remains practical for manufacturing.
What industries use precision optical prisms?
Precision optical prisms are used in laser systems, automotive optics, semiconductor equipment, consumer optical products, scientific instruments, measurement systems, imaging devices, surveying equipment, and industrial inspection systems.
How can a manufacturer improve prism consistency?
Consistency is improved through stable material sourcing, controlled fixturing, documented grinding and polishing processes, calibrated inspection equipment, coating-process control, operator training, traceability, statistical monitoring, and corrective-action procedures.
What information should be included in an inquiry?
An inquiry should include a drawing, prism type, material preference, dimensions, angular tolerances, wavelength, coating requirements, surface-quality standards, clear aperture, environmental conditions, quantity, delivery expectations, and inspection-documentation requirements.
Why are ISO and automotive quality certifications valuable?
Certifications such as ISO9001, ISO14001, and IATF16949 provide structured frameworks for quality management, environmental control, process documentation, risk management, corrective action, and continual improvement. They support reliable production but should be considered together with product-specific technical capability and inspection results.
Can one supplier support both prototype and volume production?
A manufacturer with engineering resources, a broad production base, and experience in multiple industries can often support the transition from prototype development to volume production. The process should be confirmed during the quotation and technical-review stages.
Conclusion
Precision optical prisms are essential components for controlling light in compact, stable, and high-performance optical systems. Their applications extend from laser optics and automotive sensors to semiconductor equipment, consumer devices, scientific instruments, and industrial measurement systems. Their advantages include compact beam folding, stable angular deviation, image rotation, wavelength separation, efficient use of total internal reflection, and reliable passive operation.
The quality of an optical prism depends on much more than its basic shape. Material selection, geometry, grinding, polishing, edge finishing, cleaning, coating, inspection, and packaging must all be controlled as part of an integrated process. A technically capable manufacturer can provide better consistency, more effective engineering support, and stronger long-term supply reliability than a general glass processor.
Changzhou Haolilai Photo-Electricity Scientific and Technical Co., Ltd. brings together experience dating from 1998, a large production facility, more than 300 employees, technical research centers, international supply experience, multiple patents and certificates, and certifications including ISO9001:2015, ISO14001:2015, and IATF16949. These strengths support the production of precision optical prisms for demanding laser, automotive, semiconductor, consumer, and scientific applications.
For customers seeking optical prisms, the most effective approach is to provide a complete technical specification and select a supplier capable of supporting design review, process development, quality control, coating, inspection, and repeat production. With the right material, geometry, surface treatment, and manufacturing discipline, an optical prism can improve the compactness, stability, accuracy, and reliability of an entire optical system.
References
1. Optical Society of America, Handbook of Optics, Optical Materials and Components.
2. Eugene Hecht, Optics, principles of geometrical and physical optics.
3. ISO 10110, Optics and photonics — Preparation of drawings for optical elements and systems.
4. ISO 9001:2015, Quality management systems — Requirements.
5. ISO 14001:2015, Environmental management systems — Requirements with guidance for use.
6. IATF 16949, Quality management system requirements for automotive production and relevant service parts organizations.
7. Optical Society of America, Applied Optics and Optical Engineering reference materials.
8. Standard terminology and inspection practices for optical surfaces, coatings, transmission, reflection, and dimensional accuracy.
 苏公网安备32041102000130号