 Search
 en
 English
 日本語
 русский
 Español
 Deutsch
 中文简体
Content
- 1 What Is an Optical Prism?
- 2 Principal Optical Prism Types
- 3 Key Performance Characteristics
- 4 Advanced Manufacturing Process
- 5 Manufacturing Strengths That Improve Customer Value
- 6 Comparison with Less Specialized Suppliers
- 7 Applications of Precision Optical Prisms
- 8 How to Specify an Optical Prism
- 9 Quality Assurance and Inspection Considerations
- 10 Advantages of Working with an Established Manufacturer
- 11 Development and Procurement Workflow
- 12 Environmental and Reliability Considerations
- 13 Sustainability and Responsible Manufacturing
- 14 Questions and Answers
- 14.1 What is the main purpose of an optical prism?
- 14.2 How is a prism different from a mirror?
- 14.3 Which materials are used to manufacture optical prisms?
- 14.4 Why are prism angles so important?
- 14.5 Can optical prisms be customized?
- 14.6 What coating should be used on an optical prism?
- 14.7 What information should be included in a quotation request?
- 14.8 How does manufacturing experience affect prism quality?
- 14.9 Are certifications important when selecting a prism supplier?
- 14.10 How should optical prisms be packaged?
- 14.11 Can one manufacturer support both prototypes and volume production?
- 15 Conclusion
- 16 References
- 17 Product: Optical prism
Optical prisms are precision components that control, redirect, separate, fold, or transform light without relying on complex moving mechanisms. Although a prism may appear to be a simple transparent block, its performance depends on highly controlled geometry, material quality, surface condition, coating technology, and inspection accuracy. In demanding applications such as laser systems, automotive optical modules, semiconductor equipment, imaging instruments, and consumer devices, a small angular or surface error can affect the entire optical system.
Modern optical prism manufacturing therefore requires much more than cutting and polishing glass. It involves optical design, material selection, precision grinding, fine polishing, edge treatment, cleaning, coating, measurement, process control, and reliable packaging. Each stage contributes to the final performance of the component. A high-quality prism must maintain the required angular deviation, transmission, reflection, image orientation, beam displacement, or dispersion characteristics throughout its service life.
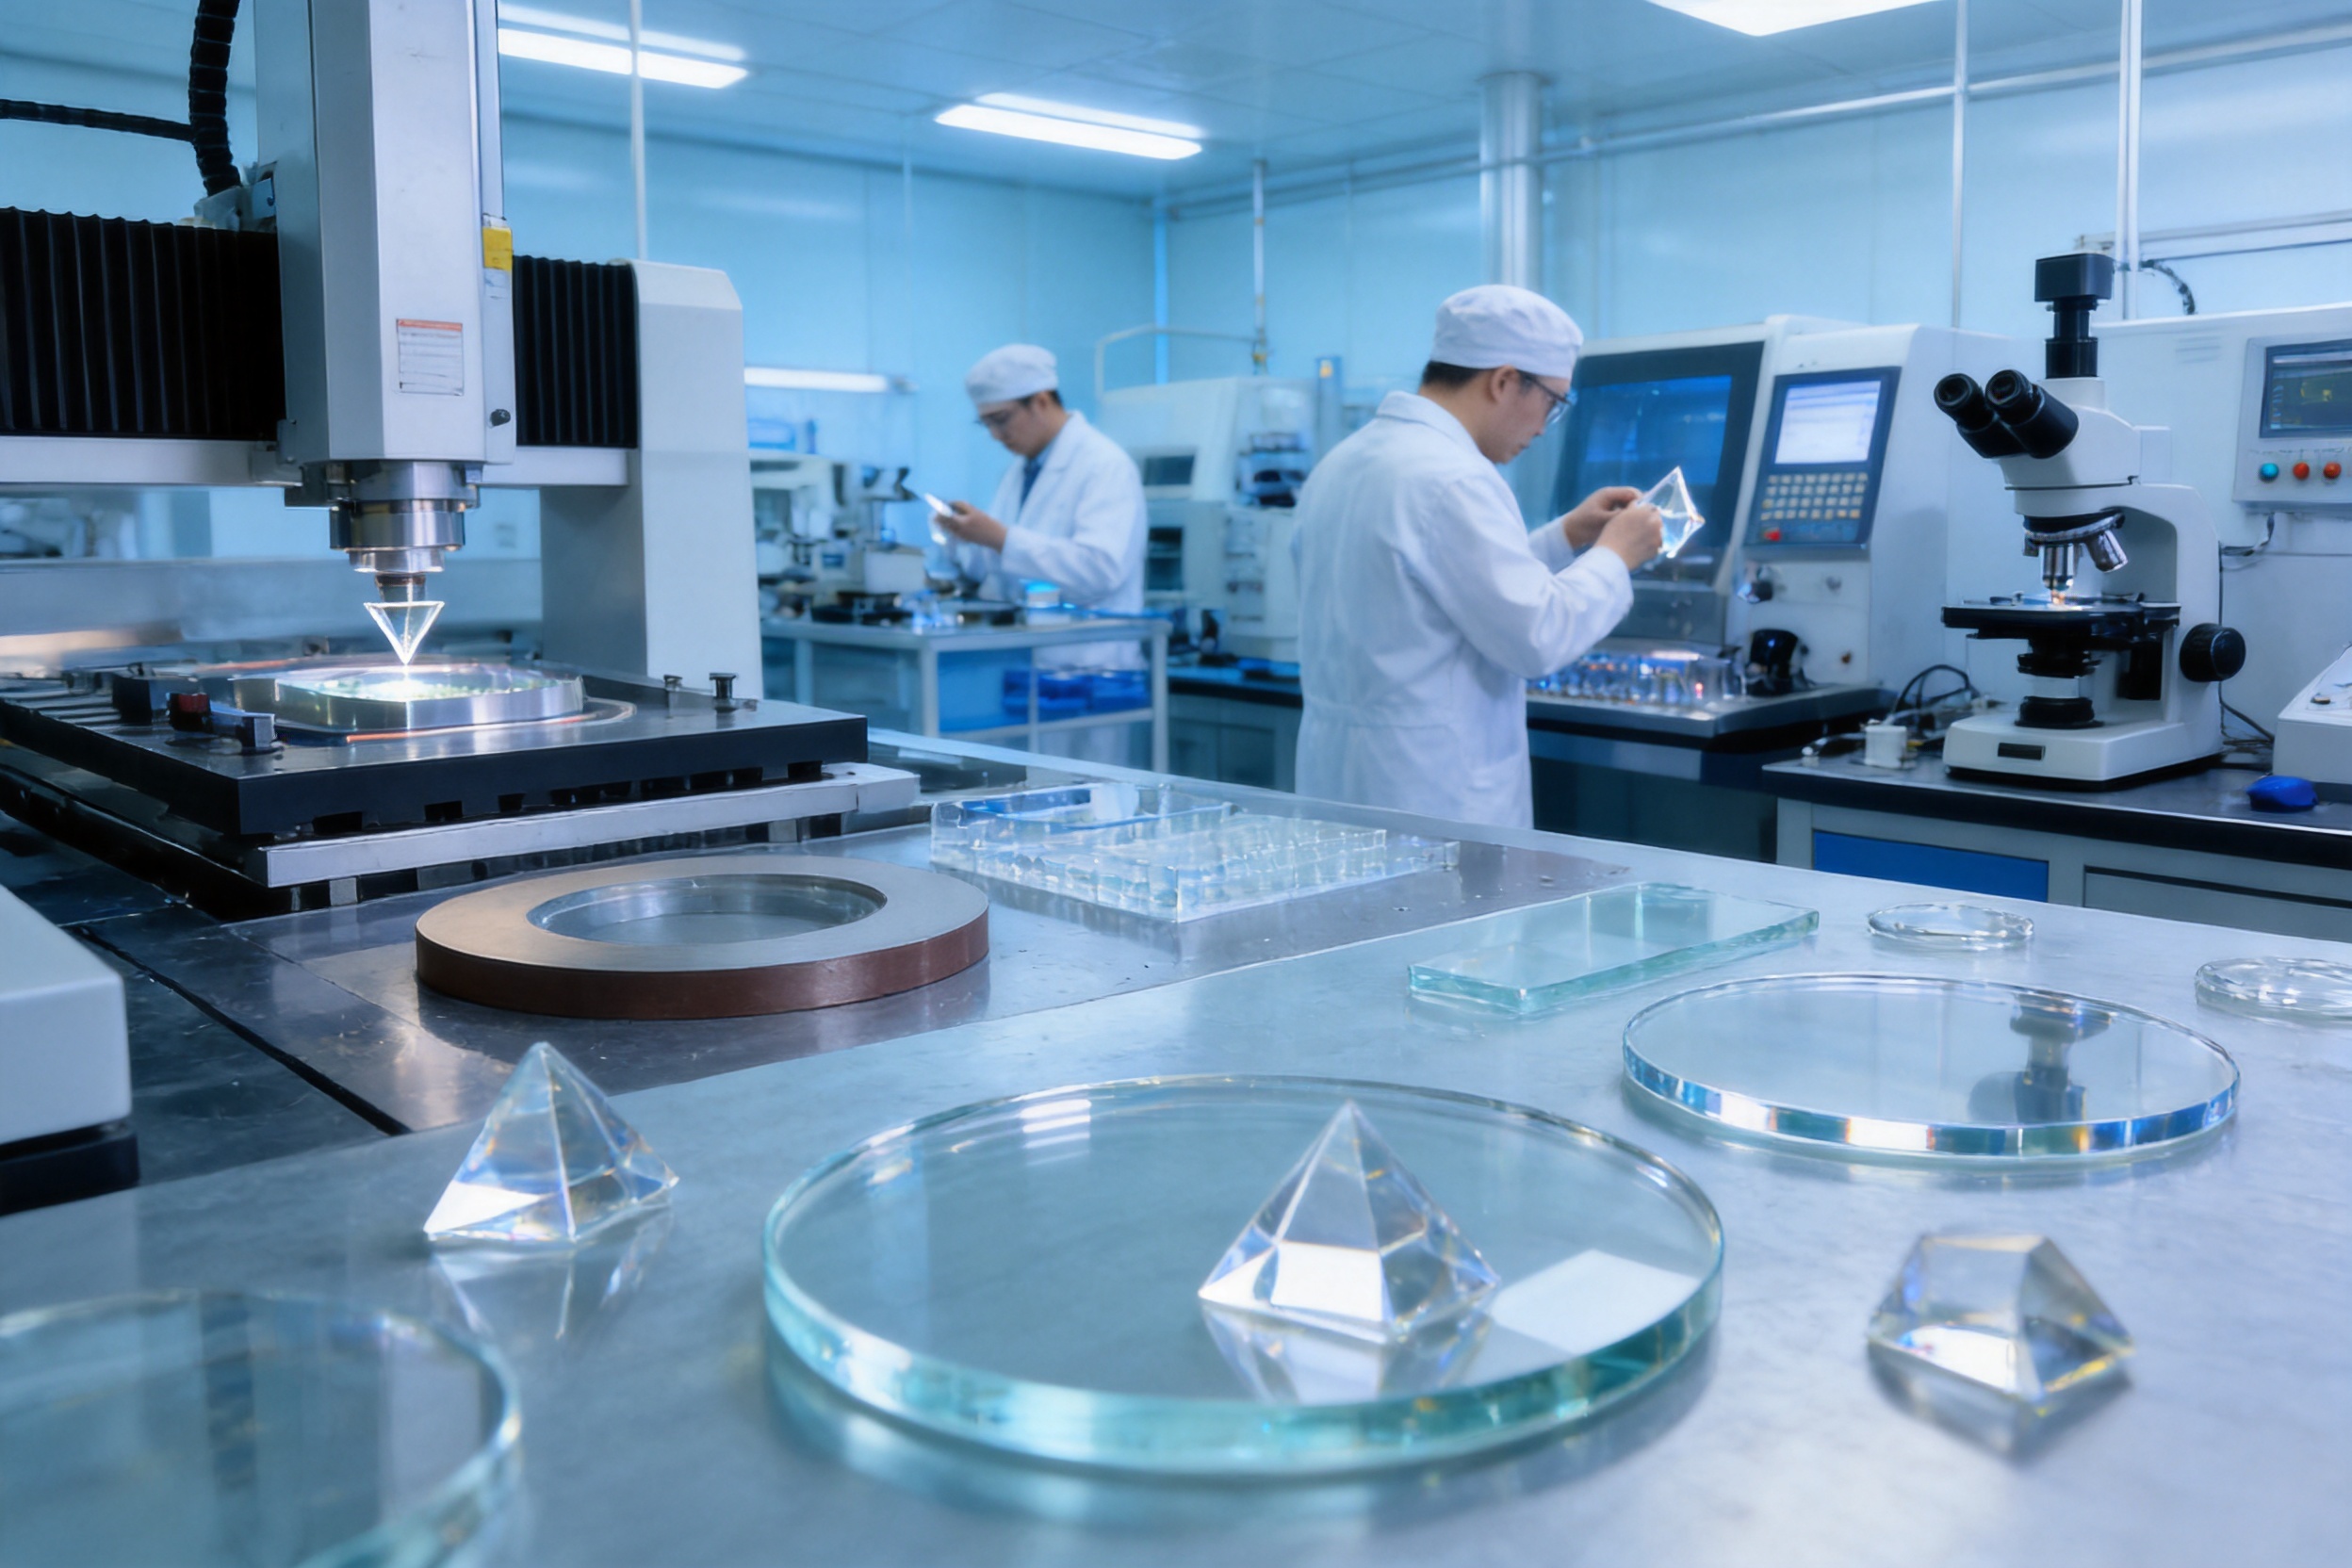
Changzhou Haolilai Photo-Electricity Scientific and Technical Co., Ltd. is an experienced Chinese manufacturer of precision optical components, including optical prisms for industrial and commercial applications. Founded in 1998, the company operates from a 35,000-square-meter facility in Changzhou, Jiangsu, and has more than 300 employees. Its capabilities cover laser optics, automotive optics, semiconductor optics, and consumer optics. These application areas require different optical materials, dimensional tolerances, coatings, and inspection standards, giving the manufacturer broad experience in developing and producing customized optical components.
This article explains the structure, functions, advantages, manufacturing process, quality controls, applications, and purchasing considerations associated with precision optical prisms. It also examines how an established optical component manufacturer can provide advantages over less specialized suppliers through process integration, engineering experience, certification, and production consistency.
What Is an Optical Prism?
An optical prism is a transparent optical component with two or more precisely oriented surfaces that transmit or reflect light. Most optical prisms are manufactured from optical glass, fused silica, or other transparent materials with carefully controlled refractive properties. When light enters a prism, its direction changes according to refraction, reflection, or a combination of both.
The optical behavior of a prism is determined by several factors. These include the refractive index of the material, the angle between the optical surfaces, the wavelength of the incident light, the angle of incidence, and the condition of each surface. A prism can deviate a light beam, reverse an image, rotate an image, separate wavelengths, produce internal reflection, or create a controlled beam offset.
Unlike a conventional lens, which primarily focuses or diverges light through curved surfaces, a prism generally uses plane surfaces and controlled angular relationships. This makes prisms particularly useful where an optical system needs compact beam folding, image orientation, or angular correction. Their flat surfaces can also make certain designs easier to integrate into compact optical assemblies.
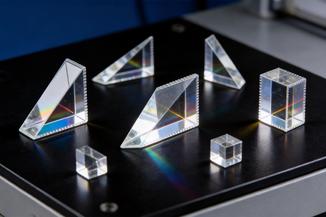
There are many types of optical prisms. Right-angle prisms are commonly used for beam deviation and total internal reflection. Dove prisms can invert or rotate images. Porro prisms are frequently used in binocular and imaging systems. Roof prisms provide compact image erection in viewing instruments. Dispersing prisms separate white light into its component wavelengths. Wedge prisms introduce a small controlled beam deviation, while retroreflecting prisms return incident light toward its source under specific conditions.
Because different prism geometries perform different optical functions, selecting the correct type requires a clear understanding of the optical path and the required system performance. A component manufacturer with experience in multiple application sectors can help customers select a suitable configuration rather than treating every prism as a standard catalog item.
Principal Optical Prism Types
Right-Angle Prisms
Right-angle prisms have two perpendicular legs and a hypotenuse surface. Depending on the optical design, the hypotenuse may be used for transmission or coated reflection, while the internal right-angle face may generate total internal reflection. These prisms can turn a beam by 90 degrees or provide compact folding within an instrument.
The main advantages of a right-angle prism include a simple geometric form, high mechanical stability, and efficient use of space. They are frequently used in laser assemblies, alignment systems, measurement instruments, and imaging devices. The accuracy of the 90-degree relationship is particularly important because angular error can change the position of the redirected beam.
Wedge Prisms
A wedge prism has two plane optical surfaces that are not parallel. It produces a controlled angular deviation rather than a symmetric beam path. Wedge prisms are used for beam steering, alignment correction, optical scanning, range-finding, and compensation of small system errors.
Wedge angle tolerance is a critical specification. A small change in wedge angle can cause a measurable change in beam deviation. For this reason, wedge prisms require careful grinding, polishing, angular measurement, and orientation control. Customized wedge prisms can be manufactured for specific wavelength ranges, deviation angles, and mounting requirements.
Dispersing Prisms
Dispersing prisms separate light into different wavelengths because the refractive index of an optical material varies with wavelength. They are used in spectroscopic equipment, optical measurement systems, educational instruments, and some laser applications.
Performance depends on the dispersion characteristics of the selected material, the prism angle, surface quality, and the wavelength range. The prism must also have adequate transmission for the intended spectrum. Material selection is therefore an important part of the design process, especially when the component is required to operate in ultraviolet, visible, or infrared bands.
Roof and Image-Erecting Prisms
Roof prisms and other image-erecting prisms are designed to change the orientation of an image while maintaining a compact optical path. They are used in observation instruments, imaging assemblies, cameras, and precision viewing devices.
These prisms require particularly careful control of roof geometry and angular alignment. Small errors between roof surfaces can introduce image doubling, contrast loss, or other visual defects. High-quality polishing and precise inspection are essential when a prism is used in an image-forming optical system.
Retroreflecting and Corner-Cube Prisms
Retroreflecting prisms are designed to return incident light toward its source or a predictable location. Corner-cube configurations use multiple mutually oriented surfaces to produce this effect over a range of incident angles.
These components are applied in surveying, distance measurement, laser ranging, industrial sensing, and scientific instruments. The accuracy of the geometric relationships among the reflecting surfaces determines the quality of the retroreflection. Surface coatings may be added when total internal reflection is insufficient for the intended operating conditions.
Custom Optical Prisms
Many optical systems require prisms that do not fit a standard shape. Custom components may include special apertures, truncated corners, mounting flats, nonstandard angles, multiple coated surfaces, or complex dimensional relationships. They may also require a particular glass type, transmission band, environmental durability, or low-scatter finish.
A custom prism program normally begins with a technical drawing or optical specification. The manufacturer evaluates the design, confirms material availability, identifies critical tolerances, and develops a manufacturing and inspection plan. This process helps avoid problems such as excessive edge stress, inaccessible polishing surfaces, coating shadowing, or measurement difficulties.
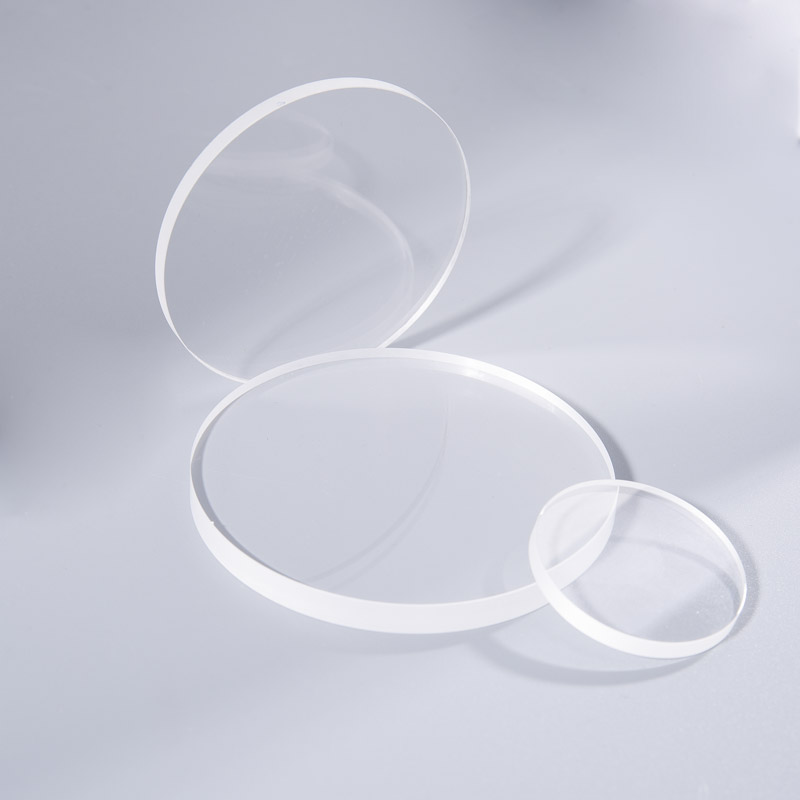
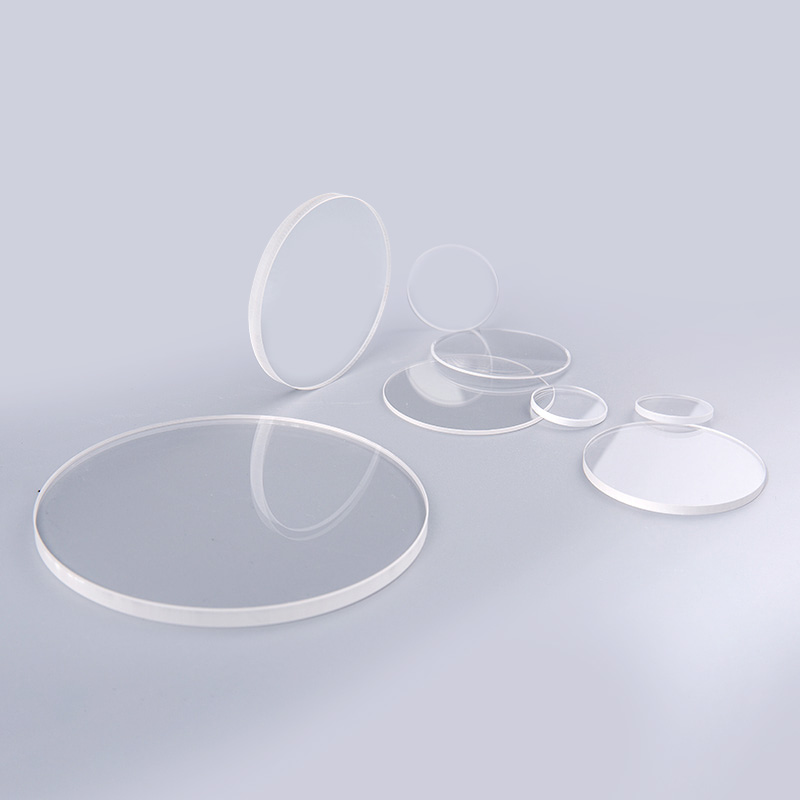
Optical prism
Key Performance Characteristics
The performance of an optical prism is defined by a combination of optical, mechanical, and environmental characteristics. A component should not be evaluated only by its external appearance or nominal dimensions. The most important requirements depend on the intended application.
Material and Refractive Index
Optical glass selection affects refraction, dispersion, transmission, thermal behavior, and chemical durability. Different glass families offer different refractive indices and Abbe numbers. A high-index material can provide greater angular deviation in a compact design, while a low-dispersion material may be preferred when chromatic separation must be minimized.
For ultraviolet or high-power laser applications, fused silica may be selected because of its transmission, low thermal expansion, and resistance to certain forms of radiation. For visible imaging systems, optical glass may provide the required balance of refractive index, homogeneity, transmission, and cost. The final choice should be based on the full optical and environmental specification rather than a single material property.
Surface Flatness and Surface Quality
Surface flatness describes how closely a polished surface conforms to the intended plane. Surface quality generally refers to visible scratches and digs or other localized surface defects. These characteristics influence wavefront distortion, scattering, contrast, and transmission.
High-performance laser and imaging applications often require tighter surface specifications than general illumination or simple beam-folding applications. However, tighter specifications can increase processing time, inspection requirements, and cost. A practical supplier should help the customer establish an appropriate specification instead of automatically recommending unnecessarily strict values.
Angular Accuracy
The angles between prism surfaces determine beam deviation, image orientation, and assembly alignment. Angular accuracy is therefore one of the most important parameters in prism production. A prism with excellent surface polish may still fail if its geometric angles are incorrect.
Angular tolerances may be specified in arcminutes, arcseconds, or another suitable unit. The required accuracy depends on the optical system. Precision measurement instruments and controlled fixturing are necessary to verify these relationships. Consistent angular inspection also helps identify process drift before large quantities are completed.
Clear Aperture and Edge Quality
The clear aperture is the usable optical area through which light passes without unacceptable obstruction or defects. It must be considered together with edge thickness, chamfers, bevels, and mounting features. A prism can meet its overall size specification but still be unsuitable if its clear aperture is too small for the system beam.
Edges are vulnerable during grinding, polishing, cleaning, coating, and handling. Proper edge treatment reduces chipping and improves safety during assembly. At the same time, chamfers must not intrude into the active aperture. The correct balance between protection and optical area should be defined in the technical drawing.
Transmission and Reflection
Uncoated optical glass reflects a portion of incident light at each air-glass interface. Anti-reflection coatings can reduce this loss and improve transmission over a selected wavelength band. Reflective coatings can be applied where a prism surface is intended to redirect light through external reflection rather than total internal reflection.
Coating selection depends on wavelength, angle of incidence, polarization, laser power, environmental conditions, and expected service life. A coating optimized for visible light may not perform well in the near-infrared or ultraviolet range. A professional manufacturer should review the complete optical path before recommending a coating.
Homogeneity, Bubbles, and Inclusions
Material homogeneity affects wavefront quality, particularly in precision imaging and laser applications. Bubbles, inclusions, striae, and internal stress can scatter light or cause local optical distortion. Material inspection and appropriate quality grading are therefore important when a prism will be used in a sensitive optical path.
Advanced Manufacturing Process
Precision prism production is a sequence of controlled operations. Each operation establishes the conditions required for the next one. The manufacturing process may vary according to the material, shape, size, tolerance, coating, and quantity, but the main stages remain broadly similar.
1. Technical Review and Optical Design Confirmation
Production begins with an engineering review of the customer’s drawing, three-dimensional model, or optical requirements. The review considers prism type, material, dimensions, angles, clear aperture, surface quality, flatness, chamfers, coating requirements, inspection standards, and packaging needs.
This stage is important because some requirements may conflict. For example, a very small edge chamfer may preserve aperture but increase chipping risk, while a very large chamfer may simplify handling but reduce usable optical area. Similarly, a coating specification may need to account for the actual incidence angle rather than only the nominal wavelength.
Engineering review also helps determine whether the design is suitable for batch manufacturing. Fixtures, reference surfaces, polishing access, measurement datum points, and process sequence are evaluated before production starts. This reduces the risk of late modifications and improves repeatability.
2. Optical Material Preparation
Suitable optical material is selected according to the required refractive index, dispersion, transmission range, thermal properties, and environmental resistance. Material blanks are inspected and prepared for cutting. At this stage, the manufacturer may consider internal homogeneity, visible inclusions, strain, and other quality indicators.
Material traceability is valuable for demanding applications. Recording material information and processing batches supports later analysis if a question arises about optical performance or environmental durability. It also helps maintain consistency when repeat orders are produced over an extended period.
3. Cutting and Rough Shaping
The material blank is cut into a rough prism shape with allowance for later grinding and polishing. Cutting parameters must be selected to minimize chipping, cracking, and unnecessary material loss. The rough shape should provide enough stock for precision correction while remaining efficient to manufacture.
For complex or small components, fixturing and orientation are especially important. Poor support can produce stress or movement during machining. A stable process at this stage improves the accuracy of subsequent surface generation.
4. Precision Grinding
Grinding establishes the basic geometry of the prism. Abrasive tools remove material and bring surfaces closer to the final dimensions and angles. Coarse grinding provides efficient stock removal, while finer grinding reduces subsurface damage and prepares the component for polishing.
The grinding sequence must account for the relationship between all optical surfaces. If one reference surface is established incorrectly, the error may transfer to the other faces. Controlled datum selection and frequent measurement help maintain the intended prism geometry.
Precision grinding is also used to produce wedges, right angles, roof features, and other critical forms. The process must balance removal rate with geometric stability. Excessive grinding force or heat can contribute to stress, deformation, or edge damage.
5. Fine Grinding and Lapping
Fine grinding and lapping improve surface condition and dimensional accuracy before final polishing. These operations reduce the depth of subsurface damage created during rough grinding. They also help establish a more uniform surface texture.
Flatness and angle control become increasingly important during this stage. Depending on the component design, the manufacturer may use dedicated tooling, controlled abrasive sizes, and carefully selected support methods. Process parameters are adjusted to suit the material and the required surface geometry.
6. Polishing
Polishing produces the transparent optical surface required for efficient transmission, reflection, and imaging. It removes the remaining fine damage and creates a smooth surface with low scatter. The polishing method must preserve the geometric accuracy achieved during grinding.
Polishing a prism is more complex than polishing a simple round lens because multiple flat surfaces and angular relationships must be maintained. A polishing tool that improves one surface can influence the alignment or support condition of another. Operators and process engineers must therefore manage contact pressure, polishing time, slurry condition, part support, and reference orientation.
For high-quality optical components, polishing is followed by careful inspection under suitable illumination. Surface defects, edge chips, haze, stains, and residual marks are assessed against the agreed specification. If necessary, the process is adjusted and the component is returned for additional correction.
7. Edge Treatment and Cleaning
After optical surfaces are polished, edges are treated to reduce sharpness and protect against handling damage. Chamfers or bevels must remain within the defined dimensions and must not reduce the active aperture beyond the permitted limit.
Cleaning removes polishing residues, particles, oils, and other contaminants. Optical cleaning is performed with methods compatible with the material and coating requirements. Cleanliness is especially important before coating because contamination can reduce adhesion, create pinholes, or cause visible defects.
8. Optical Coating
Coating processes may be used to improve transmission, increase reflection, reduce ghost images, or protect a surface. Anti-reflection coatings are commonly selected for transmitting surfaces, while reflective coatings may be applied to surfaces designed to redirect light.
Coating design is determined by the wavelength range, incidence angle, polarization condition, substrate material, and environmental requirements. A multilayer dielectric coating may be appropriate for demanding laser or imaging applications. Other designs may be selected for broader spectral coverage or specific cost and durability targets.
Before coating, components are carefully cleaned and inspected. Fixtures must expose the intended surfaces while protecting areas that should remain uncoated. After coating, the surfaces are checked for uniformity, adhesion, visual defects, and performance against the agreed requirements.
9. Final Measurement and Documentation
Final inspection confirms that the completed prism meets dimensional, angular, optical, surface, and coating requirements. Depending on the order, inspection may include dimensions, angles, flatness, surface quality, clear aperture, transmission, reflectance, coating appearance, and environmental test results.
Measurement data and inspection records support product traceability and customer confidence. For repeated production, historical data can also reveal trends in process capability. This information is useful for improving fixtures, refining process parameters, and maintaining stable quality from batch to batch.
Manufacturing Strengths That Improve Customer Value
The principal advantage of an experienced optical prism manufacturer is not simply access to machines. It is the combination of engineering knowledge, process control, inspection capability, trained personnel, and application understanding. These strengths reduce technical risk and improve the probability that the component will perform as expected in the customer’s assembly.
Integrated Technical Expertise
A manufacturer with a long history in precision optics can evaluate the relationship between optical design and production reality. This is important when a component contains multiple tight tolerances or when the prism is part of a compact assembly. Early engineering feedback can identify risks that may not be obvious from a two-dimensional drawing.
Changzhou Haolilai Photo-Electricity Scientific and Technical Co., Ltd. has developed technical centers focused on precision optical lenses and enterprise technology research. These facilities support product development, process improvement, and technical problem solving. The company has also obtained invention patents, utility model patents, and Jiangsu High and New Tech Products, indicating continued investment in optical engineering and production technology.
Experience Across Multiple Markets
Optical prisms for laser equipment have different requirements from prisms used in automotive optical modules or consumer imaging devices. Laser components may require high damage resistance, low scatter, and strict wavefront control. Automotive components may need environmental durability, stable performance over temperature variation, and compatibility with compact assemblies. Semiconductor applications may emphasize cleanliness, repeatability, and precision alignment.
Experience across laser, automotive, semiconductor, and consumer optics allows a manufacturer to understand these different priorities. It also supports the development of flexible manufacturing methods for various sizes, materials, coatings, and quantities.
Quality Management and Certification
Quality management systems provide a framework for controlling documents, processes, inspection, corrective actions, and continual improvement. The company holds ISO9001:2015 and ISO14001:2015 certifications, as well as IATF16949 certification. These certifications are particularly relevant to customers seeking controlled production, environmental management, and automotive-quality processes.
Certification does not replace product-specific inspection, but it strengthens the organizational system used to manage quality. It can also simplify supplier evaluation for customers whose procurement procedures require recognized management standards.
Production Scale and Capacity
A 35,000-square-meter operating area and a workforce of more than 300 employees provide a foundation for organized production and technical specialization. Scale can support separate functions for engineering, production, quality, procurement, and customer service. It may also make it easier to coordinate prototype development with later volume production.
Production scale should not be confused with automatic superiority. The important question is whether capacity is supported by stable processes and effective inspection. When these elements are combined, a larger technical organization can provide better continuity, repeatability, and response to engineering changes than a small supplier with limited resources.
International Supply Experience
The company exports to more than 20 countries and holds more than 30 certificates and patents. International supply experience generally requires attention to packaging, documentation, communication, technical drawing interpretation, export coordination, and customer-specific quality requirements.
For buyers of optical prisms, this experience can reduce the administrative and technical friction associated with overseas sourcing. Clear specifications, sample approval, inspection records, and consistent communication are important factors in a successful supply relationship.
Comparison with Less Specialized Suppliers
| Evaluation Area | Specialized Precision Optical Manufacturer | General Glass or Basic Machining Supplier |
|---|---|---|
| Optical surface control | Processes are developed for flatness, surface quality, scatter, and optical performance. | May focus mainly on visual appearance or general dimensional accuracy. |
| Angular accuracy | Prism angles and reference relationships are planned and measured as optical requirements. | Angles may be treated primarily as mechanical dimensions. |
| Material selection | Material is matched to wavelength, refractive index, dispersion, and environmental conditions. | Material choice may be based mainly on availability or price. |
| Coating capability | Coatings can be selected and controlled according to wavelength, incidence angle, and application. | Coating options may be limited or outsourced without complete process integration. |
| Application support | Engineering teams can review optical paths, tolerances, and assembly risks. | Support may be limited to producing the supplied shape. |
| Quality systems | Formal quality and environmental systems support traceability and corrective action. | Inspection and documentation practices may vary between orders. |
| Production continuity | Established processes and technical resources support prototypes and repeat orders. | Repeatability may depend heavily on individual operators or subcontractors. |
The comparison demonstrates why optical prisms should be purchased from a supplier that understands optical performance as well as mechanical production. A general glass processor may produce a visually acceptable component, but the finished prism may not provide the required beam deviation, image quality, transmission, or environmental stability.
Applications of Precision Optical Prisms
Laser Optics
Prisms are used in laser systems for beam folding, alignment, separation, steering, and path reduction. A prism can redirect a beam within a compact enclosure and may reduce the number of mirrors required in certain designs. The choice between a prism and a mirror depends on wavelength, incidence angle, polarization, power density, packaging, and contamination risk.
Laser applications often require low absorption, high surface quality, suitable coatings, and accurate angular relationships. For high-power systems, coating damage threshold and thermal behavior must be considered. For precision measurement systems, wavefront distortion and beam pointing stability may be more important.
Automotive Optical Systems
Automotive optical modules may use prisms for sensing, illumination, display, imaging, or beam redirection. Compact packaging is a major benefit because automotive systems often have limited installation space. A prism can fold an optical path, reposition an image, or support a sensor layout that would be difficult to achieve with a straight optical axis.
Automotive components may also encounter vibration, humidity, temperature cycling, dust, and long service periods. Therefore, optical performance must be combined with suitable mechanical design, coating durability, cleanliness, and production consistency. IATF16949 certification provides a relevant quality-management foundation for automotive-related supply chains.
Semiconductor and Inspection Equipment
Semiconductor manufacturing and inspection equipment often relies on precise optical paths. Prisms may be used for beam routing, polarization control, imaging, measurement, or compact instrument design. These systems can be highly sensitive to angular drift, contamination, scattering, and wavefront error.
Stable production and thorough cleaning are important in this sector. The component must not only meet a drawing but also integrate reliably into a controlled optical assembly. Material traceability and inspection records can assist equipment manufacturers in maintaining their own process controls.
Consumer Optical Products
Consumer optical products include cameras, projectors, viewing instruments, display systems, and compact sensing devices. These products generally require a balance of performance, size, appearance, cost, and production volume.
Prisms for consumer devices may be small and produced in large quantities. Consistency is essential because even a small variation can create image misalignment, brightness differences, or assembly difficulties. A manufacturer with experience in both precision optics and scalable production can help customers maintain quality while controlling unit cost.
Scientific and Measurement Instruments
Scientific instruments use prisms for spectroscopy, beam deviation, optical referencing, polarization analysis, and image orientation. Such instruments may operate across specific wavelength bands and require carefully characterized optical properties.
In measurement systems, the prism often becomes part of the reference architecture. Its angle, material stability, and surface condition can influence the accuracy of the instrument. Engineering review and calibrated inspection are therefore important during supplier selection.
How to Specify an Optical Prism
A complete prism specification should define more than length, width, and height. The following items should be considered before requesting a quotation or approving a design.
- Prism type and optical function.
- Optical material and material grade.
- Wavelength range or operating spectrum.
- Overall dimensions and dimensional tolerances.
- Critical prism angles and angular tolerances.
- Clear aperture requirements.
- Surface flatness and surface quality.
- Chamfer or bevel dimensions.
- Coating type, wavelength range, and incidence angle.
- Reflectance or transmittance targets.
- Environmental and temperature requirements.
- Required inspection reports and traceability.
- Packaging and cleanliness requirements.
- Prototype quantity and expected annual volume.
If the optical design is still under development, the customer should provide as much information as possible about the beam path, aperture, wavelength, power, image orientation, and available space. This allows the manufacturer to recommend a practical geometry and identify any production risks at an early stage.
Drawings should clearly indicate optical surfaces, mechanical reference surfaces, datums, coating areas, and noncritical features. Ambiguous drawings can lead to unnecessary cost or inconsistent interpretation. A supplier with optical engineering experience can help convert functional requirements into measurable manufacturing specifications.
Quality Assurance and Inspection Considerations
Quality assurance for optical prisms should cover incoming material, in-process geometry, polished surfaces, coatings, final dimensions, cleanliness, and packaging. Inspection plans are normally developed according to the critical characteristics of the component.
Incoming Material Inspection
Material inspection may include visual examination, documentation review, refractive index confirmation, and assessment of internal defects. The exact method depends on the application and material grade. For sensitive components, the material must be sufficiently homogeneous and free from unacceptable bubbles, inclusions, or stress.
In-Process Inspection
In-process checks verify that the prism remains within the intended geometry during grinding, lapping, and polishing. Measuring only at the end of production can make correction more difficult and increase material waste. Regular process checks provide earlier information about tool wear, fixture changes, or parameter drift.
Final Optical Inspection
Final optical inspection may include surface quality assessment, flatness measurement, angular measurement, clear aperture verification, and transmission or reflection testing. The selected instruments and methods should be suitable for the size and specification of the prism.
Inspection lighting and cleanliness are important when evaluating scratches, digs, stains, haze, and edge defects. Visual criteria should be defined clearly so that the supplier and customer use the same acceptance standard.
Coating Inspection
Coated prisms may require checks for visual uniformity, adhesion, spectral performance, reflectance, transmittance, and environmental durability. Coating performance must be evaluated at the intended wavelength and, where relevant, at the intended angle of incidence.
Packaging and Handling
Even a perfectly manufactured prism can be damaged by poor packaging. Optical surfaces should be protected from contact, particles, moisture, and mechanical shock. Packaging materials must be compatible with cleanliness requirements and should prevent movement during transportation.
For international shipments, packaging should also account for changes in temperature and humidity. Clear labeling and batch identification help maintain traceability when multiple prism types are delivered together.
Advantages of Working with an Established Manufacturer
Choosing an established optical component manufacturer can provide several advantages compared with selecting a supplier solely on price. These advantages become more important as the prism specification becomes tighter or the component becomes critical to the final product.
First, technical communication is usually more effective. A supplier familiar with optical terminology can discuss angular deviation, wedge error, clear aperture, coating bands, and wavefront requirements without reducing the project to basic mechanical dimensions.
Second, integrated production can reduce the number of external handoffs. When cutting, grinding, polishing, cleaning, coating, inspection, and engineering support are coordinated within one organization, responsibility is clearer and process feedback can move more quickly.
Third, an experienced supplier can support design for manufacturability. Minor changes to a chamfer, reference surface, coating boundary, or tolerance may improve yield without reducing optical performance. These improvements can lower total cost and shorten delivery time.
Fourth, established quality systems support repeat orders. Optical components are often used in products that remain in production for several years. The ability to reproduce the same material, geometry, surface condition, coating, and inspection method is essential for long-term supply.
Fifth, broad application experience can help when the customer is developing a new optical product. A manufacturer active in laser, automotive, semiconductor, and consumer optics may be able to recommend suitable production approaches based on similar technical challenges encountered in other projects.
Development and Procurement Workflow
A successful optical prism project usually follows a structured sequence. The customer first defines the optical function and system constraints. The manufacturer then reviews the design, confirms material and process feasibility, and prepares a quotation based on the required tolerances and quantity.
For a new design, prototype production allows the customer to verify mechanical fit, beam path, image orientation, coating performance, and assembly method. Any changes should be recorded and incorporated into the controlled drawing or specification before volume production.
During production approval, the parties should agree on inspection criteria, sample size, documentation, packaging, and change-control procedures. If a material, coating, tool, or process parameter must change later, the change should be evaluated for its potential effect on optical performance.
Repeat orders benefit from a stable part number, revision-controlled drawing, approved inspection standard, and retained production records. This approach reduces ambiguity and helps ensure that a replacement batch performs like the original batch.
Environmental and Reliability Considerations
Optical prisms may be exposed to temperature changes, humidity, vibration, chemicals, dust, cleaning agents, and radiation. The material, coating, adhesive, mount, and packaging must be considered together. A prism that performs well in a laboratory may require additional protection for an automotive or industrial environment.
Thermal expansion can affect angular alignment and focus in precision systems. Materials with lower thermal expansion may be preferred for certain laser or measurement applications. However, the complete assembly must also be evaluated because differences between the prism, mount, and housing can create stress.
Coating durability is important where surfaces are exposed to handling, cleaning, humidity, or temperature cycling. Protective coatings, sealed assemblies, and suitable handling procedures can increase service life. The required environmental tests should reflect actual operating conditions rather than relying only on general assumptions.
Sustainability and Responsible Manufacturing
Optical manufacturing uses energy, water, abrasives, polishing compounds, cleaning chemicals, packaging materials, and other resources. Responsible production therefore requires attention to waste reduction, process efficiency, environmental control, and safe handling of materials.
ISO14001:2015 certification provides a structured framework for environmental management. It supports the identification of environmental aspects, compliance obligations, improvement objectives, and operational controls. For customers with their own sustainability programs, a supplier’s environmental management system can be an important part of the overall supply-chain evaluation.
Efficient material preparation can reduce glass waste, while process monitoring can reduce rejected components and repeated polishing. Durable packaging and properly sized protective materials can also reduce damage during transportation. Sustainability and quality are often connected because stable processes typically produce fewer rejected parts and less unnecessary consumption.
Questions and Answers
What is the main purpose of an optical prism?
An optical prism changes the path or orientation of light. Depending on its geometry, it can deviate a beam, fold an optical path, invert or rotate an image, separate wavelengths, or return light toward its source.
How is a prism different from a mirror?
A mirror redirects light primarily through reflection at a coated or reflective surface. A prism uses refraction, total internal reflection, external reflection, or a combination of these effects. A prism may offer compact geometry and multiple optical functions, while a mirror may provide simpler beam redirection in other designs.
Which materials are used to manufacture optical prisms?
Optical glass is widely used, while fused silica and other transparent optical materials may be selected for particular wavelength ranges, thermal conditions, or laser applications. The material should be chosen according to refractive index, dispersion, transmission, thermal behavior, and environmental requirements.
Why are prism angles so important?
Prism angles determine beam deviation, image orientation, and alignment within the optical system. Even a small angular error can shift a beam or create image distortion. Accurate grinding, polishing, fixturing, and measurement are therefore essential.
Can optical prisms be customized?
Yes. Prisms can be customized in material, geometry, dimensions, angles, clear aperture, chamfers, coatings, and inspection requirements. Custom design review is recommended when the prism is part of a compact or high-precision optical assembly.
What coating should be used on an optical prism?
The coating depends on wavelength, incidence angle, polarization, desired transmission or reflection, laser power, and environmental exposure. Anti-reflection coatings are used to reduce surface reflection, while reflective coatings are used when a surface must redirect light externally.
What information should be included in a quotation request?
A quotation request should include a drawing or model, prism type, material, dimensions, angle tolerances, surface requirements, clear aperture, coating specifications, wavelength, quantity, inspection requirements, and packaging expectations. Information about the intended application can also help the manufacturer recommend a suitable process.
How does manufacturing experience affect prism quality?
Manufacturing experience improves the ability to select suitable materials, control geometry, prevent edge damage, maintain polished surfaces, apply consistent coatings, and identify risks early. It also supports repeatability when the same prism must be produced over multiple batches.
Are certifications important when selecting a prism supplier?
Certifications such as ISO9001, ISO14001, and IATF16949 indicate that the supplier has formal systems for quality, environmental management, or automotive-related processes. Certifications should be considered together with product-specific technical capability and inspection results.
How should optical prisms be packaged?
Prisms should be protected from surface contact, particles, moisture, vibration, and impact. Packaging should keep components separated and stable during transportation. Clean packaging and clear batch identification are particularly important for coated or high-precision parts.
Can one manufacturer support both prototypes and volume production?
An established precision optical manufacturer can often support the complete progression from design review and prototypes to approved production and repeat orders. The customer should confirm available capacity, minimum quantities, inspection procedures, and change-control practices during the initial discussion.
Conclusion
Optical prisms are compact but highly engineered components. Their value comes from the accuracy with which they control light, not merely from their shape or transparency. Material quality, surface flatness, angular accuracy, clear aperture, coatings, cleanliness, and environmental stability all contribute to the final result.
Reliable prism production requires an integrated process covering design review, material preparation, cutting, grinding, lapping, polishing, edge treatment, cleaning, coating, inspection, and packaging. The best results are achieved when optical engineering and manufacturing engineering are considered together from the beginning of the project.
Changzhou Haolilai Photo-Electricity Scientific and Technical Co., Ltd. brings experience dating from 1998, a 35,000-square-meter production base, more than 300 employees, international export experience, and technical capabilities covering laser, automotive, semiconductor, and consumer optics. Its ISO9001:2015, ISO14001:2015, and IATF16949 certifications provide additional support for controlled production and responsible management.
For buyers seeking optical prisms, the most important decision is to select a supplier capable of meeting the complete optical specification consistently. A manufacturer with strong process integration, application knowledge, technical research resources, and formal quality systems can provide advantages over suppliers that offer only basic glass processing. By combining a clear design specification with early engineering communication and appropriate inspection, customers can obtain prisms that deliver reliable optical performance in demanding products and systems.
References
1. Optical Society of America, Handbook of Optics, optical materials and geometrical optics sections.
2. Edmund Optics, Optical Components and Optical Coatings Technical Reference Materials.
3. International Organization for Standardization, ISO 9001:2015, Quality Management Systems—Requirements.
4. International Organization for Standardization, ISO 14001:2015, Environmental Management Systems—Requirements with Guidance for Use.
5. International Automotive Task Force, IATF 16949, Quality Management System Requirements for Automotive Production and Relevant Service Parts Organizations.
6. J. E. Greivenkamp, Field Guide to Geometrical Optics, SPIE Press.
7. Daniel Malacara, Optical Shop Testing, Wiley-Interscience.
8. Eugene Hecht, Optics, principles of refraction, reflection, dispersion, and optical system design.
9. ISO 10110, Optics and Photonics—Preparation of Drawings for Optical Elements and Systems.
 苏公网安备32041102000130号